01
ERW Tube and Profile Mills
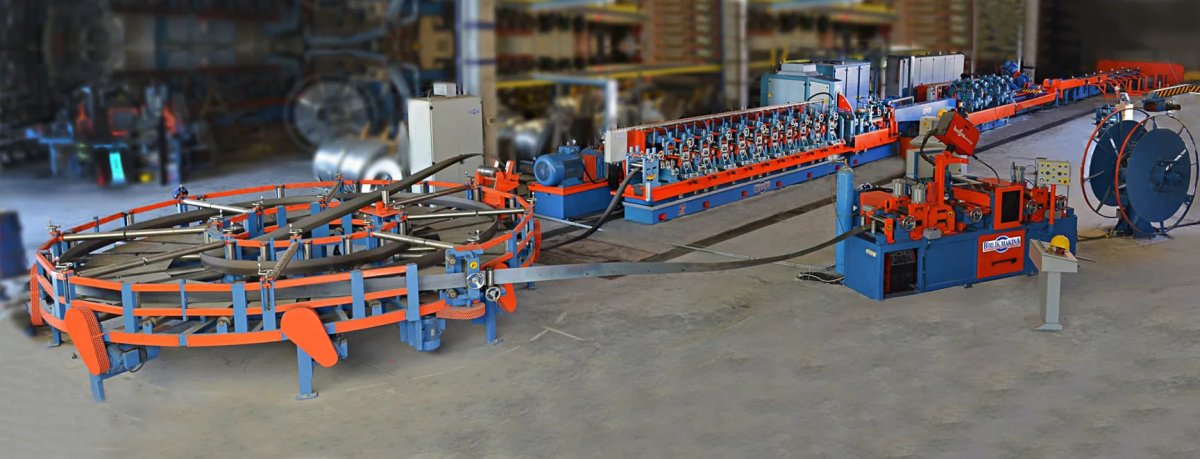
Turnkey lines for welded steel tube from Ø10 to Ø406 mm and square/rectangular profiles from 10×10 to 300×300 mm.
- Tube diameter
- Ø10 – Ø406 mm
- Wall thickness
- 0.50 – 12.70 mm
- Line speed
- up to 160 m/min
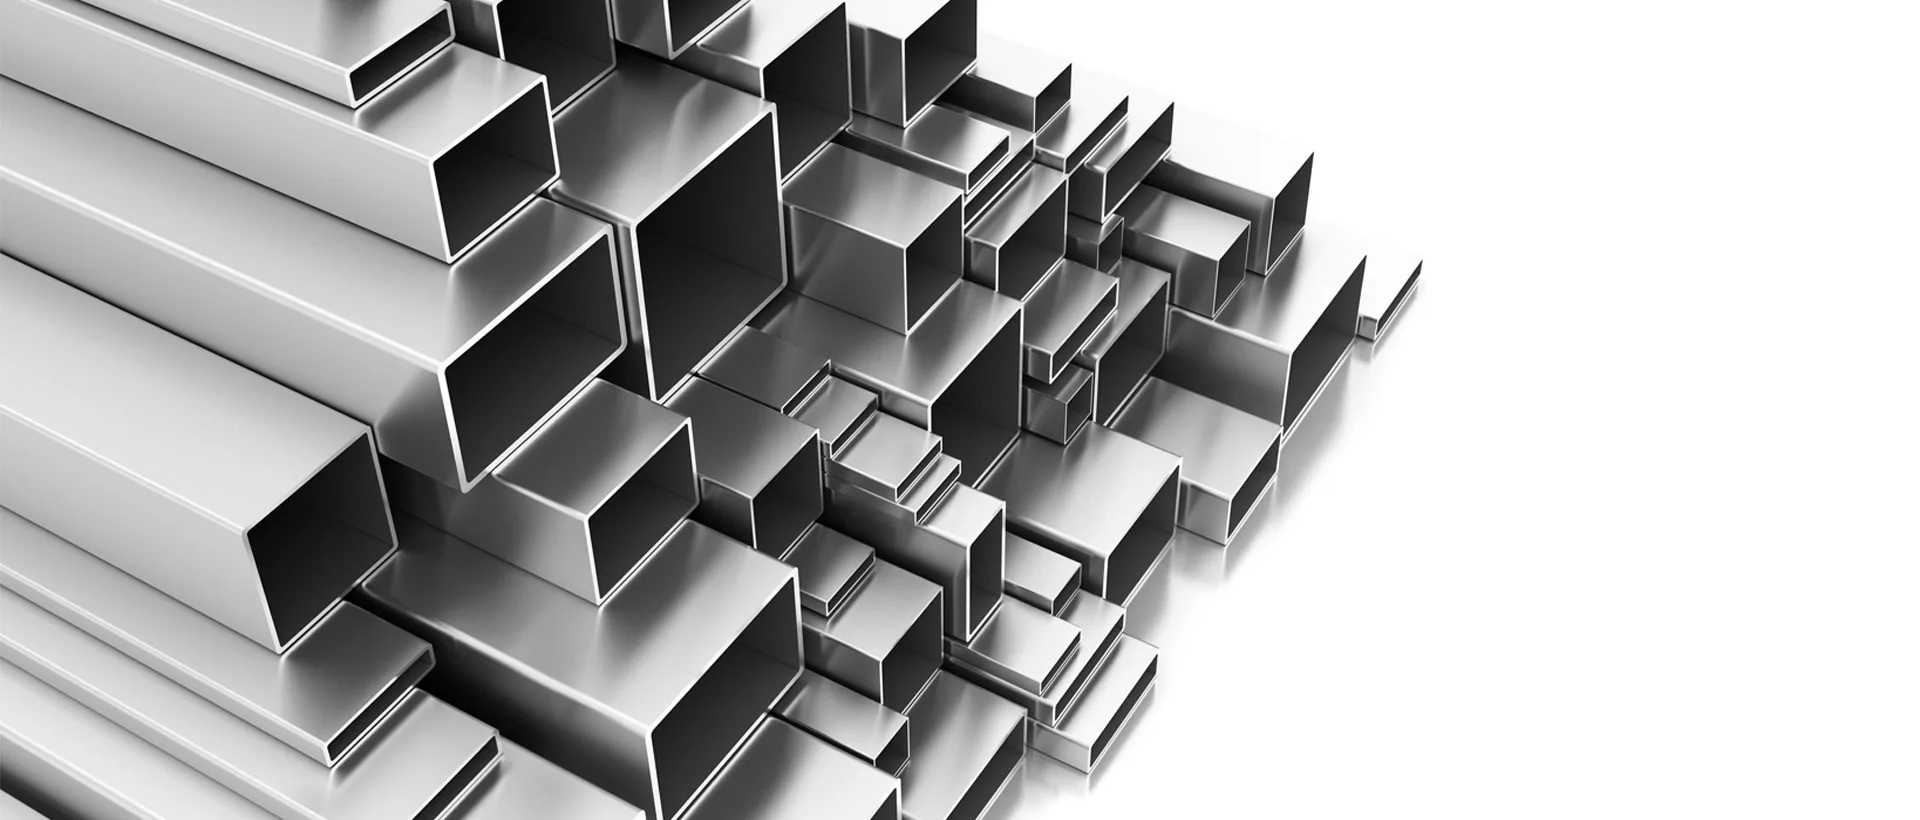
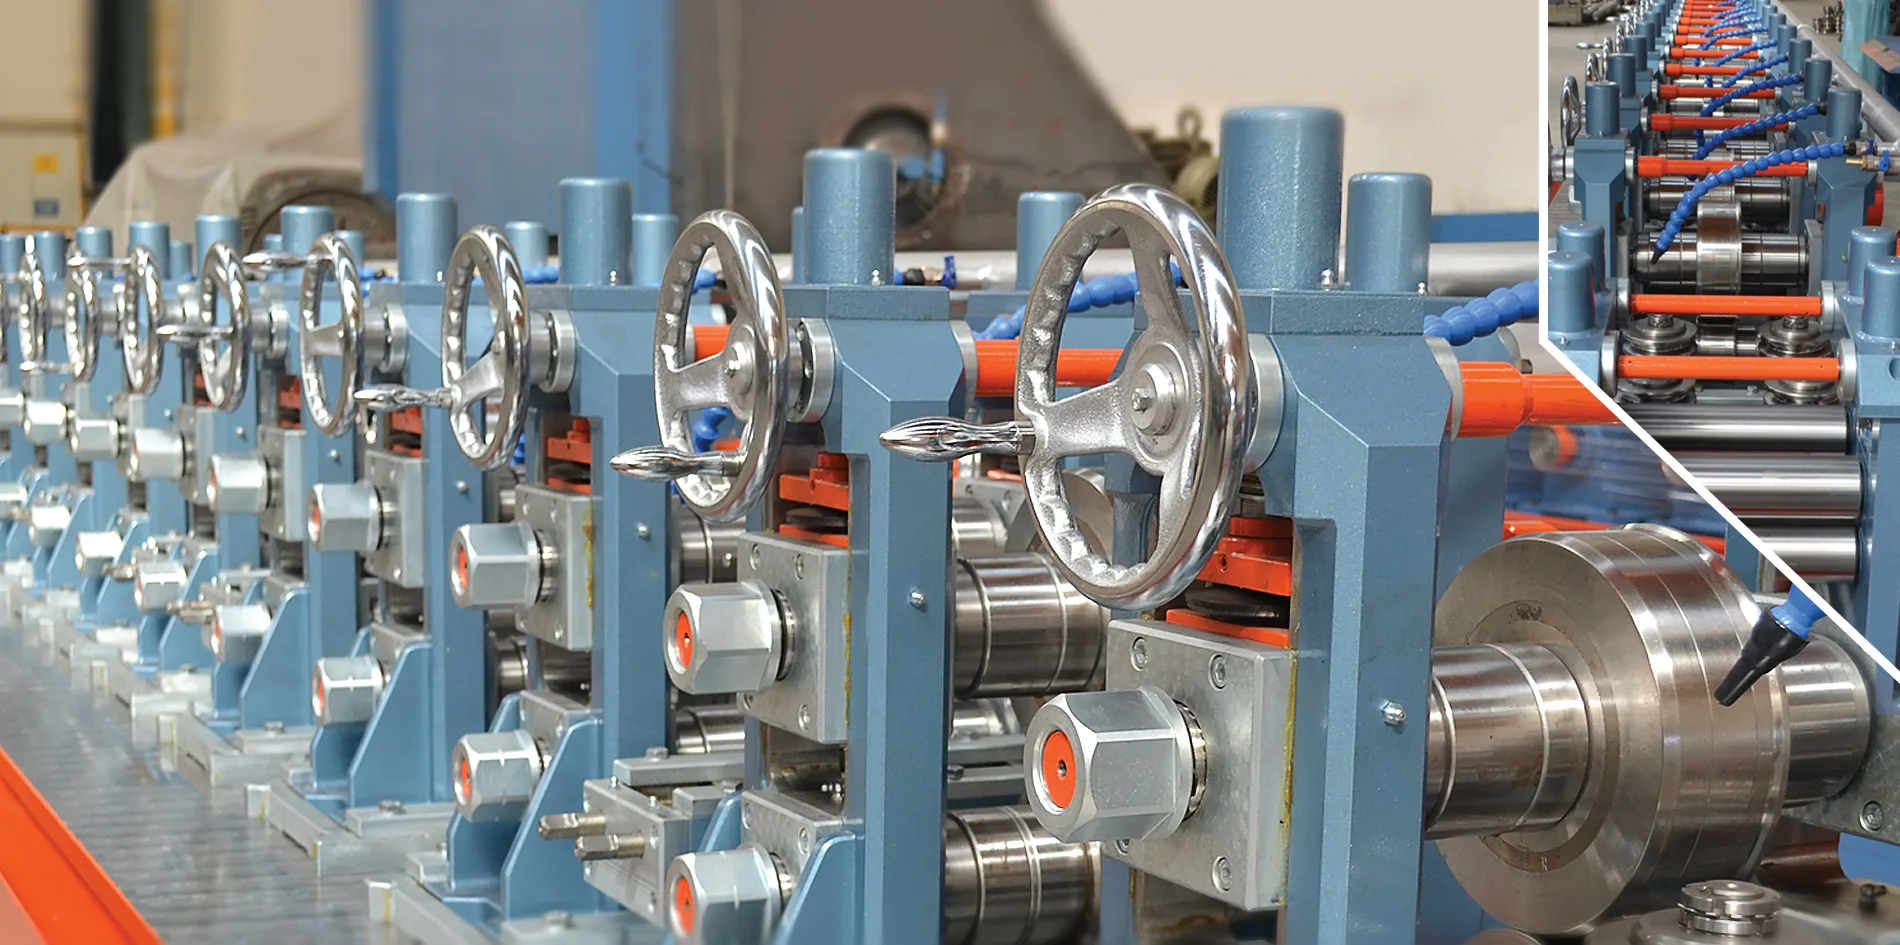
Direct forming lines that produce 20×20 – 120×120 mm square and rectangular profiles with no roll change — sizes are set from the computer.
On a direct forming line the strip is shaped straight into a square or rectangular profile, without first being formed into a round tube. Roll positions are set by computer control, so you do not need to change rolls to move to a different size.
Roll investment and set-up times are kept to a minimum, and because the same profile can be produced from a narrower strip, you also save material. The BPL series combines high speed with low operating costs.
| Model | Profile size (mm) | Wall thickness (mm) | Max. speed — S355 / St52 (m/min) | Max. speed — S245 / St37 (m/min) |
|---|---|---|---|---|
| BPL 200 | 20×20 – 50×50 | 1.10 – 2.50 | 110 | 130 |
| BPL 240 | 25×25 – 60×60 | 1.35 – 3.00 | 100 | 120 |
| BPL 320 | 30×30 – 80×80 | 1.50 – 4.00 | 90 | 105 |
| BPL 400 | 40×40 – 100×100 | 2.00 – 5.00 | 80 | 90 |
| BPL 480 | 50×50 – 120×120 | 2.00 – 6.00 | 70 | 80 |
* The machines listed are standard models; we engineer lines for the sizes and capacity you need.
Drag the plan, zoom in or tap a station. Units with photos open in detail with a single tap.
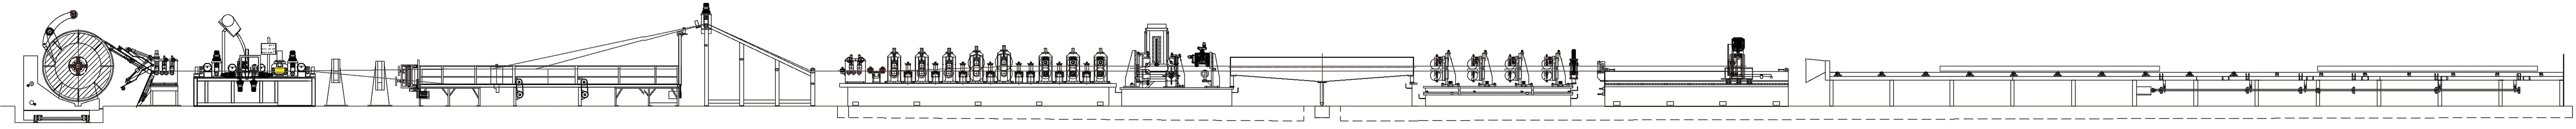
Tap a card for details on each unit.
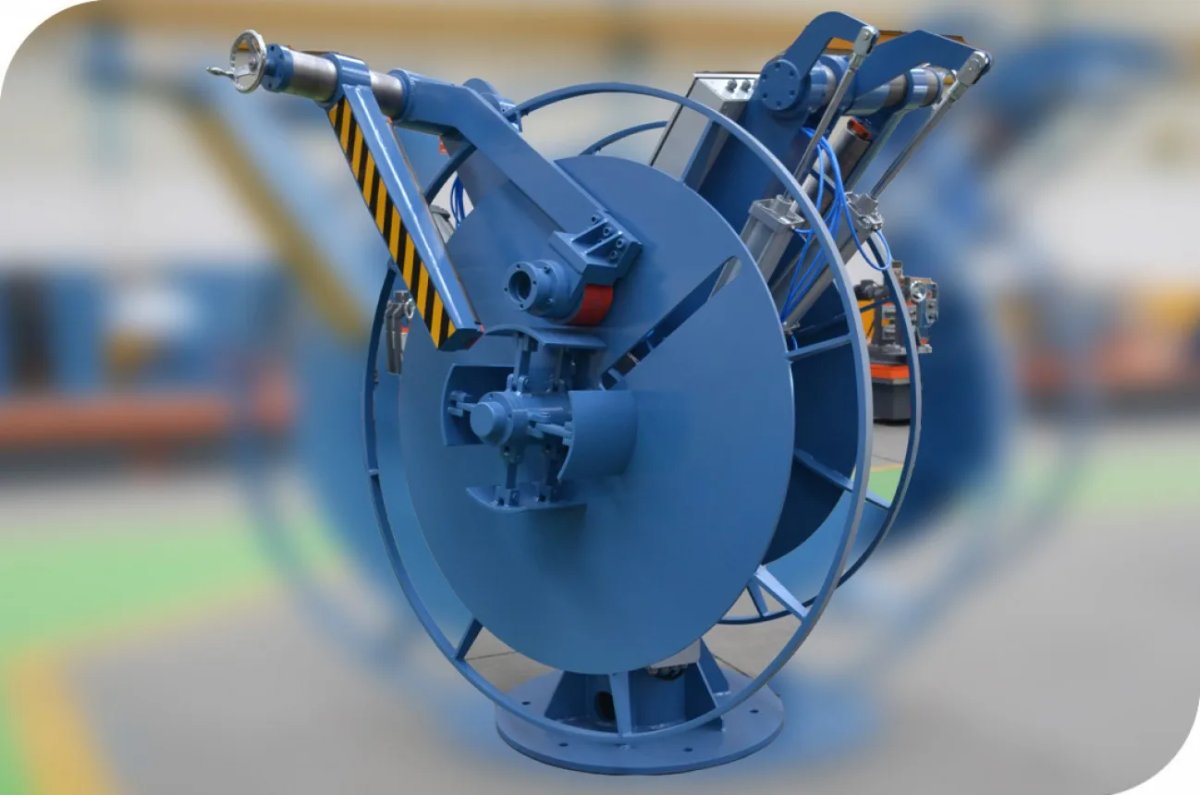
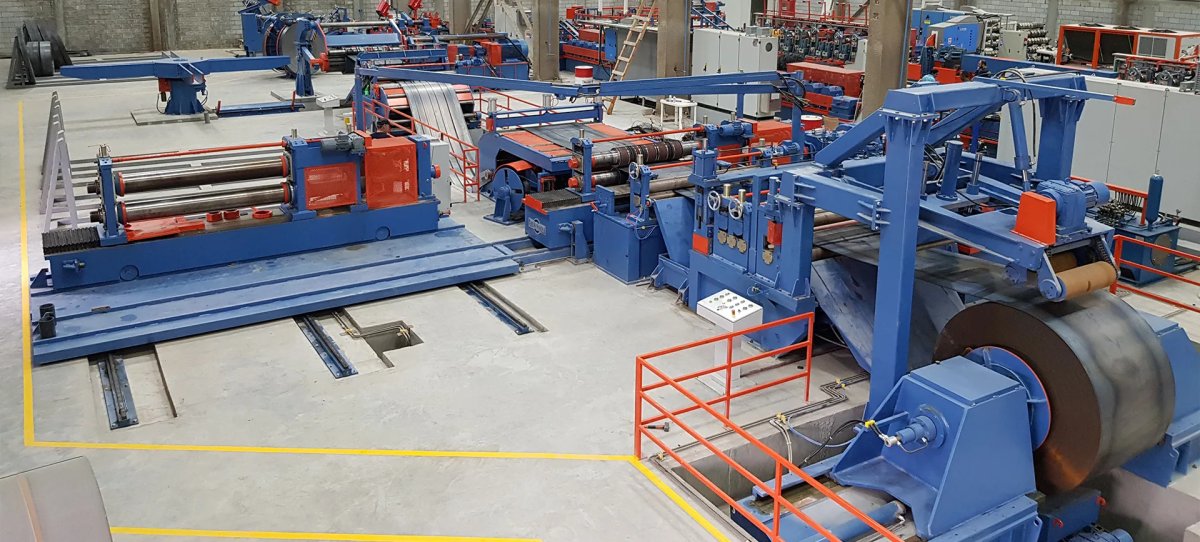
The first unit, feeding the line. Built with a single or double mandrel; on double-mandrel types a new coil is prepared on one mandrel while the other feeds the line. Coil loading, brake and hold-down roll settings are controlled by the operator.
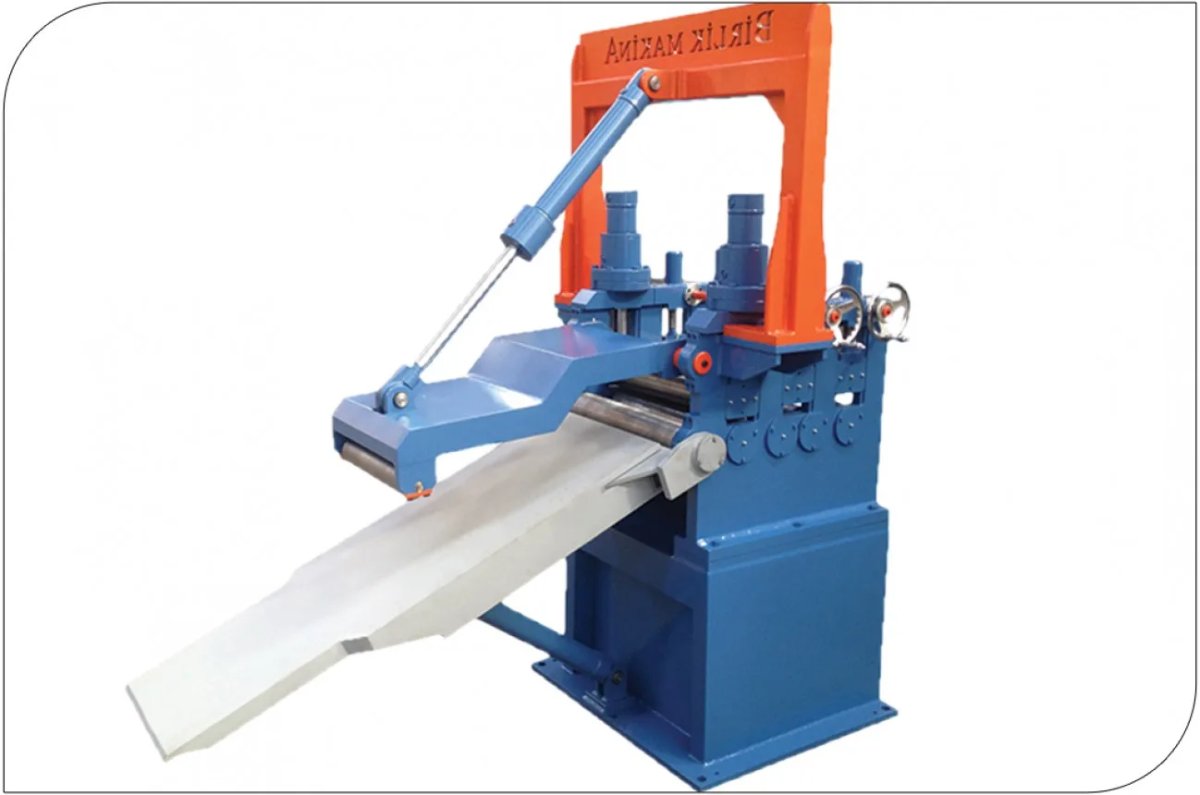
Corrects the leading end of the strip coming from the decoiler and guides it to the straightening unit for a clean entry into the line.
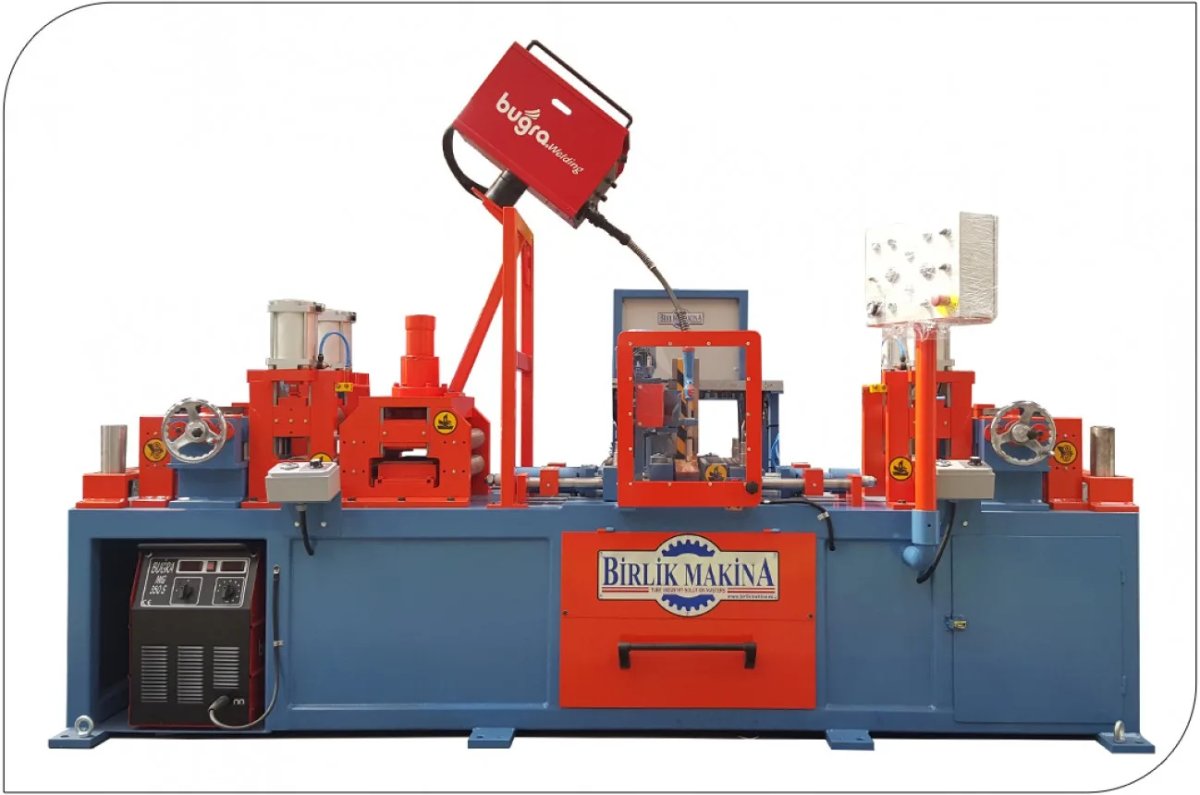
Joins the tail of the finished coil to the head of the new coil. Shearing, joining, clamping and welding are all automatic, so the line runs without interruption.
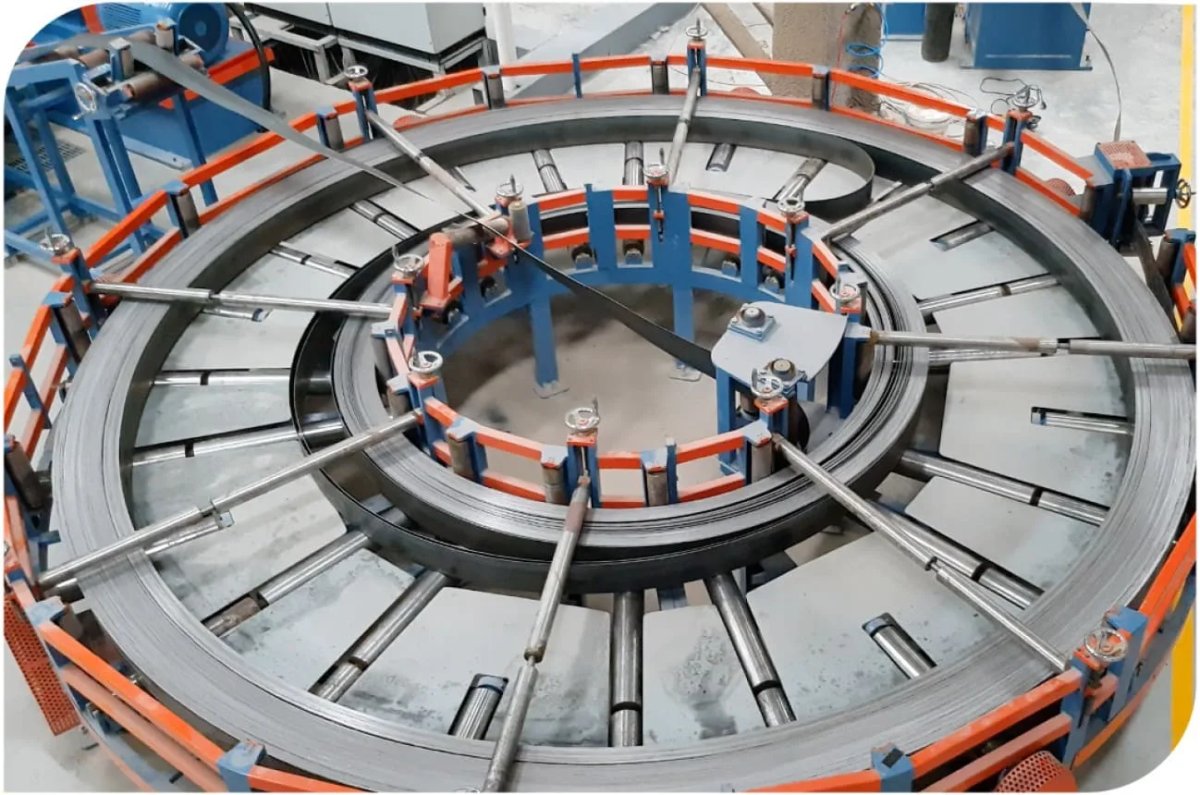
Stores strip so that the line does not stop during strip end welding, keeping the profile mill running continuously.
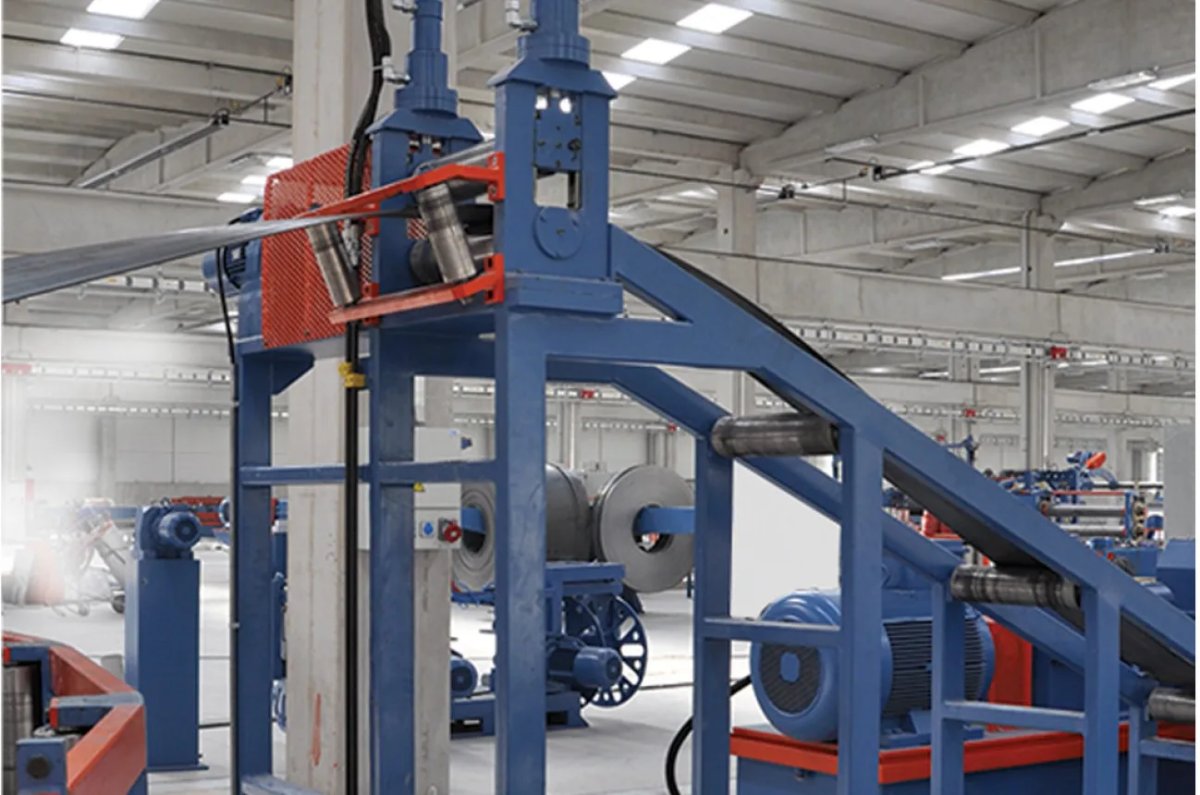
Aligns the strip coming from the accumulator and feeds it into the forming section in a controlled way.
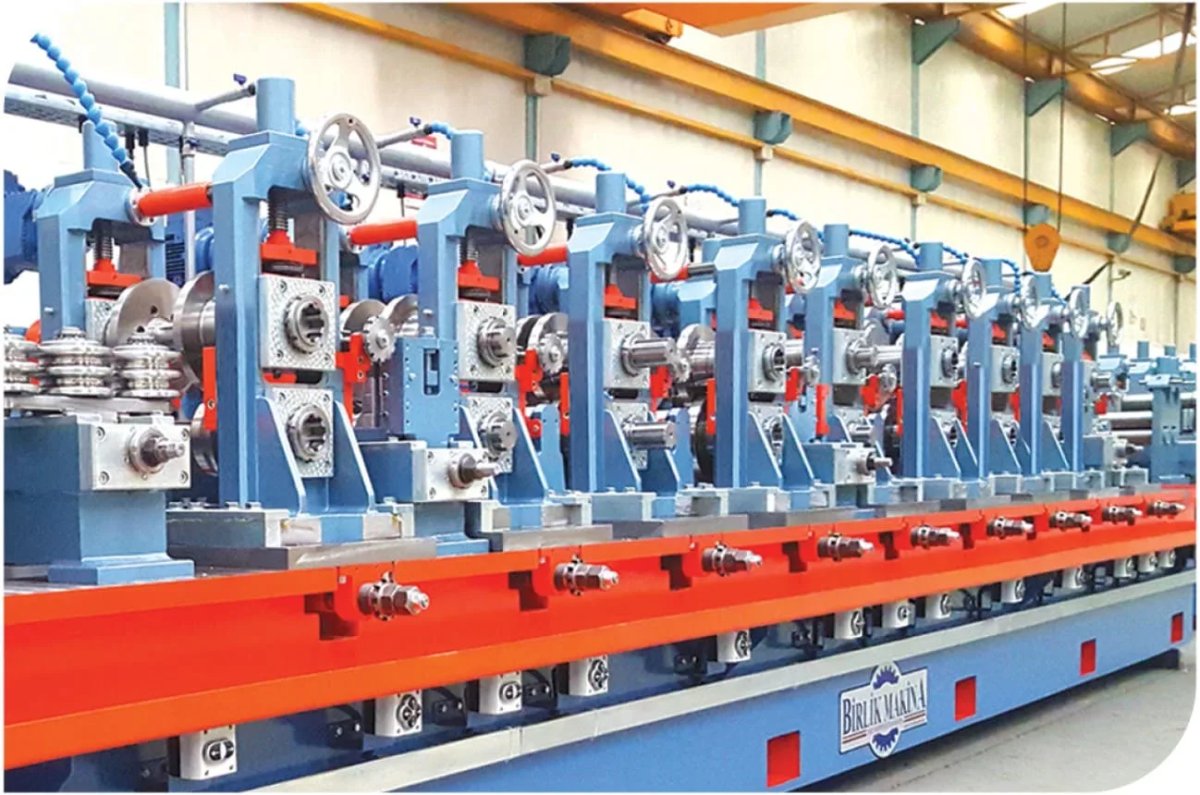
The strip is shaped directly into a square or rectangular profile without first being formed into a round tube. Because roll positions are set from the computer, no roll change is needed when the size changes.
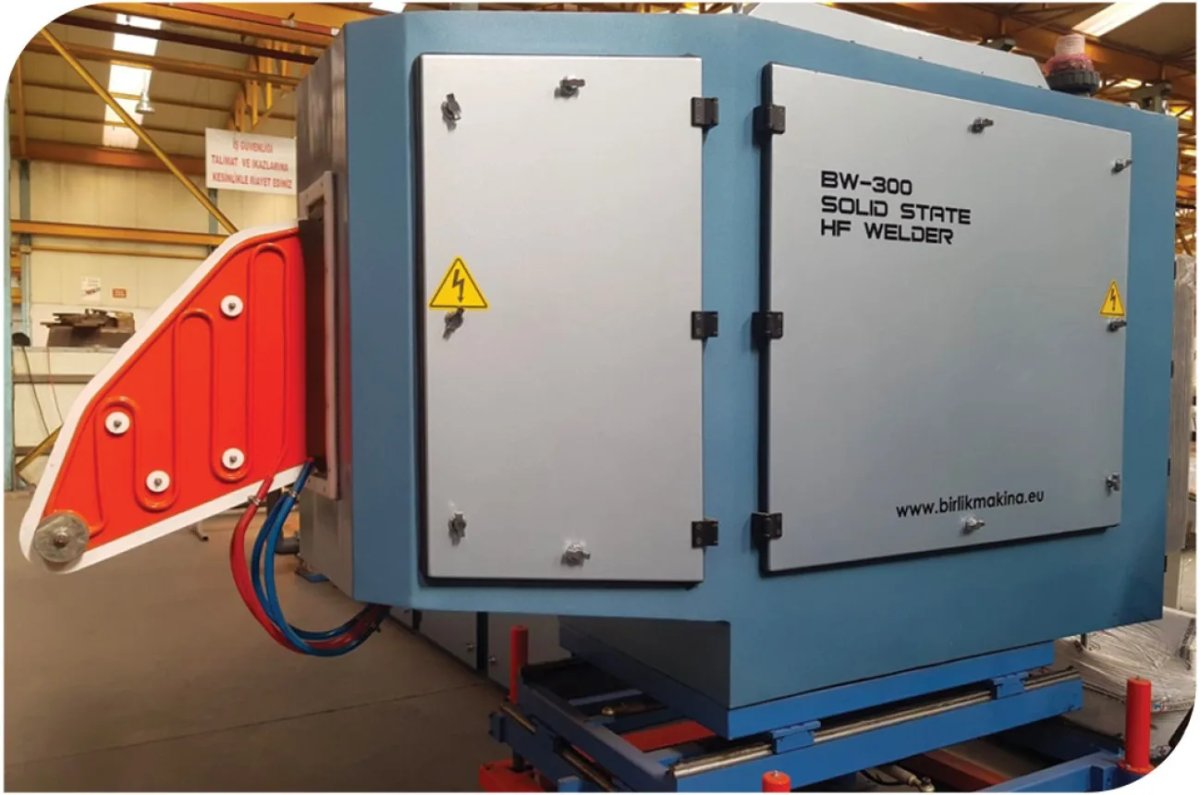
The edges of the formed strip are heated by the high-frequency welder and pressed together by squeeze rolls; the outside weld bead is removed immediately after welding.
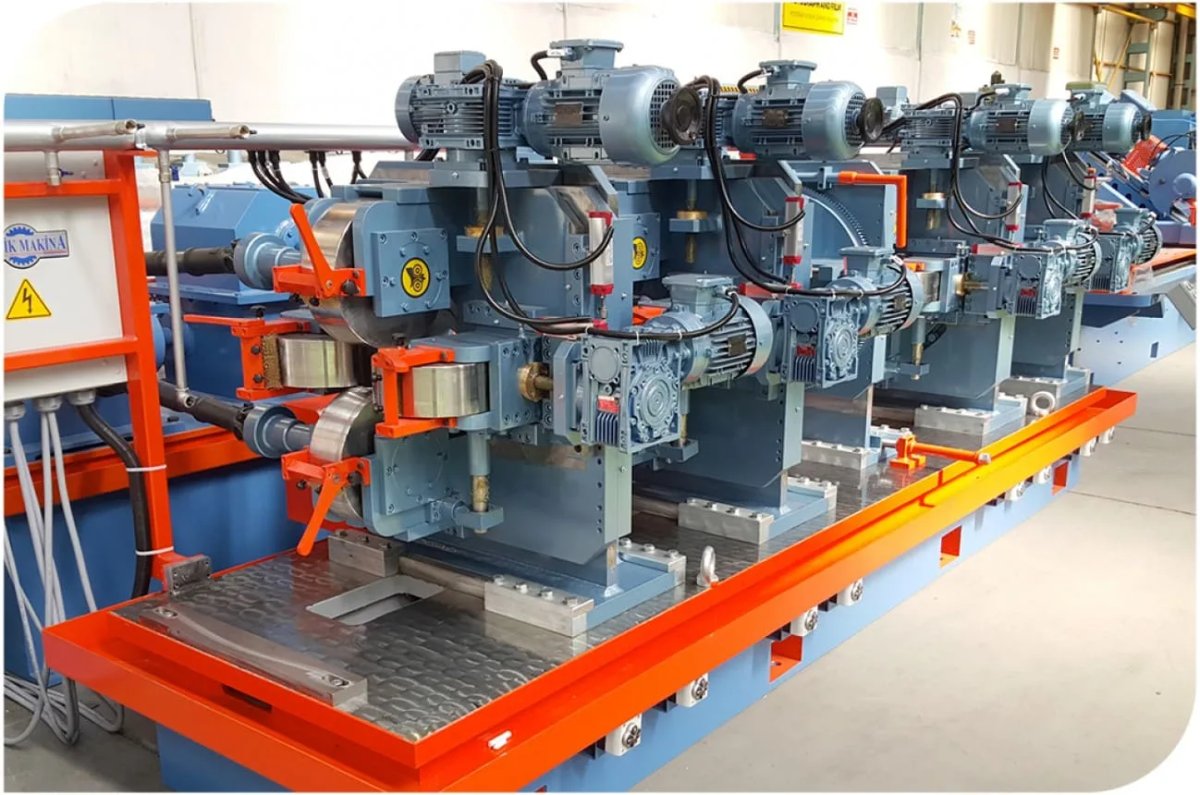
The section where the profile receives its final dimensions and corner shape, and where its straightness is corrected.
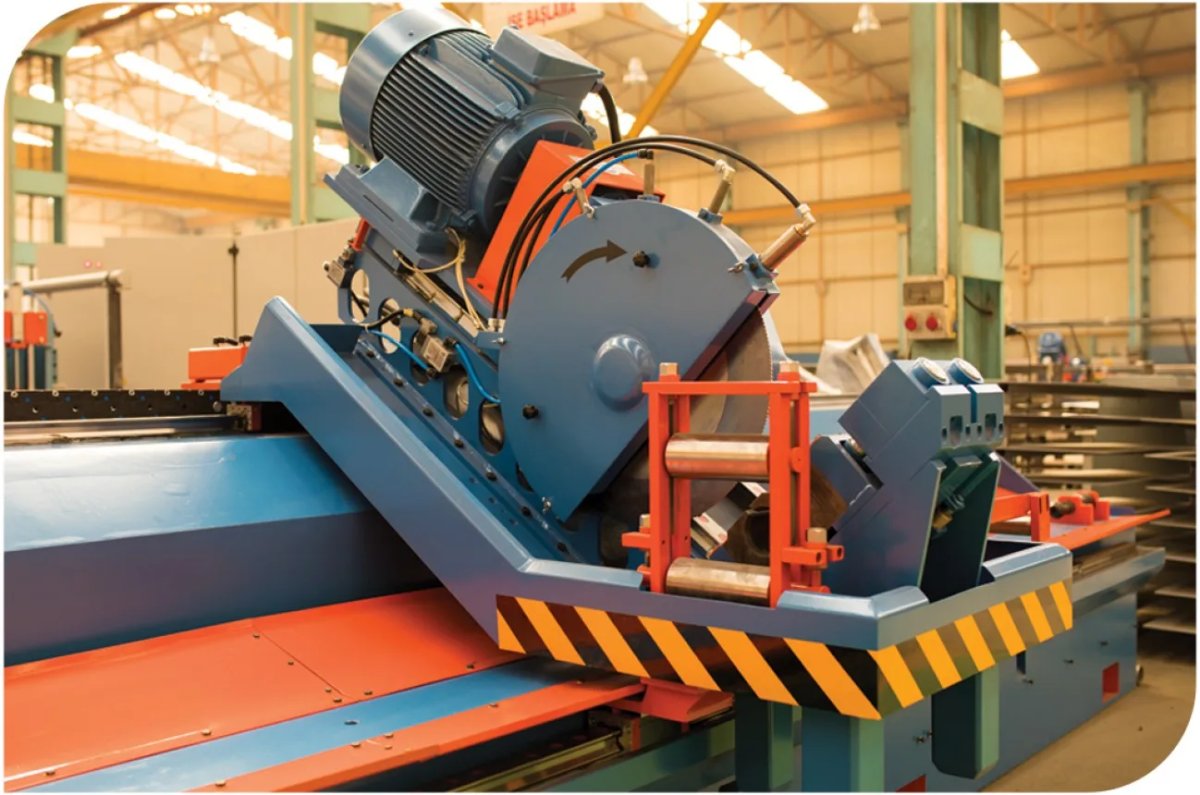
Cuts the profile to the required length without stopping the line. It travels on a linear slide and performs all functions automatically, synchronised with the line.
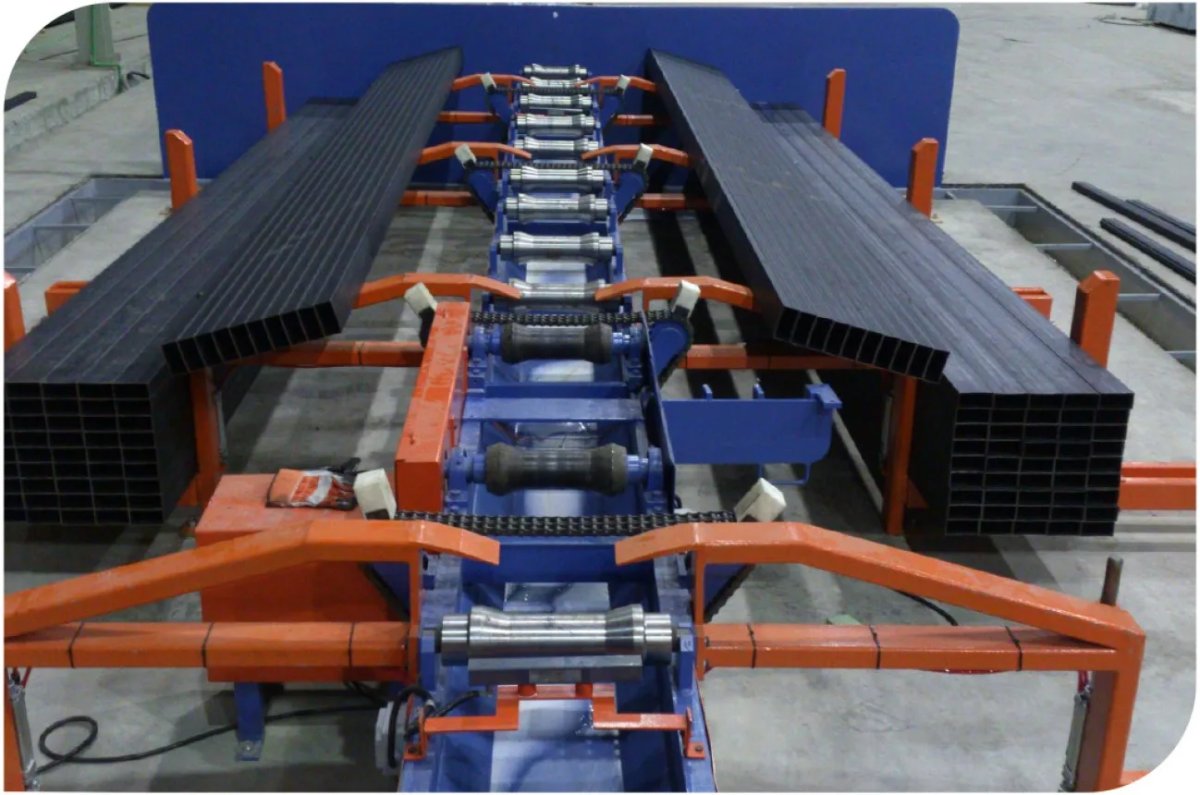
Cut profiles are carried by conveyor to the kick-off unit and packed in square bundles on both sides of the stacking table.
Share your material, product dimensions and capacity target — our engineers will prepare a technical proposal tailored to you.
On a conventional mill the strip is first formed into a round tube and then into a profile. On a direct forming line the strip is shaped straight into the profile, and size changes are made from the computer with no roll change.
The BPL series produces square and rectangular profiles from 20×20 mm to 120×120 mm, with wall thicknesses of 1.10 – 6.00 mm.
Because no separate roll set is needed for each size, roll investment and stock costs drop significantly, and set-up time is kept to a minimum.
Turnkey lines for welded steel tube from Ø10 to Ø406 mm and square/rectangular profiles from 10×10 to 300×300 mm.
Slitting lines with optional double slitter head that cut 0.50 – 12.00 mm coils up to 2000 mm wide into strips of the required width.
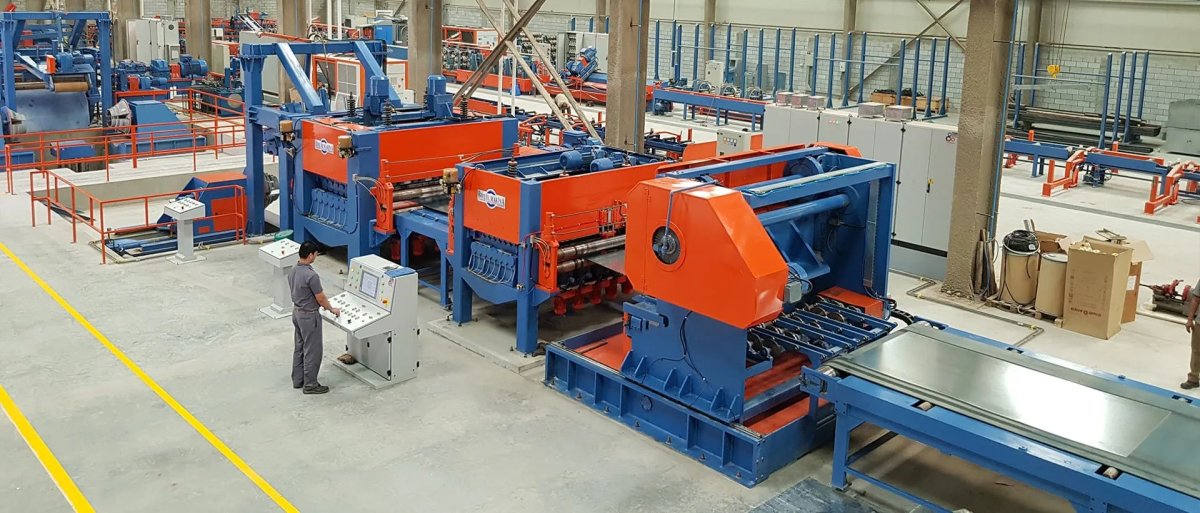
Cut-to-length lines that level 0.50 – 16.00 mm coils, cut them to the required length without stopping, and stack the sheets automatically.
Share your material, product dimensions and capacity target — our engineers will prepare a technical proposal tailored to you.