ERW Tube and Profile Mills
Turnkey lines for welded steel tube from Ø10 to Ø406 mm and square/rectangular profiles from 10×10 to 300×300 mm.
- Tube diameter
- Ø10 – Ø406 mm
- Wall thickness
- 0.50 – 12.70 mm
- Line speed
- up to 160 m/min
- Standard models
- 13 models (BTM 100 – BTM 1275)
Overview
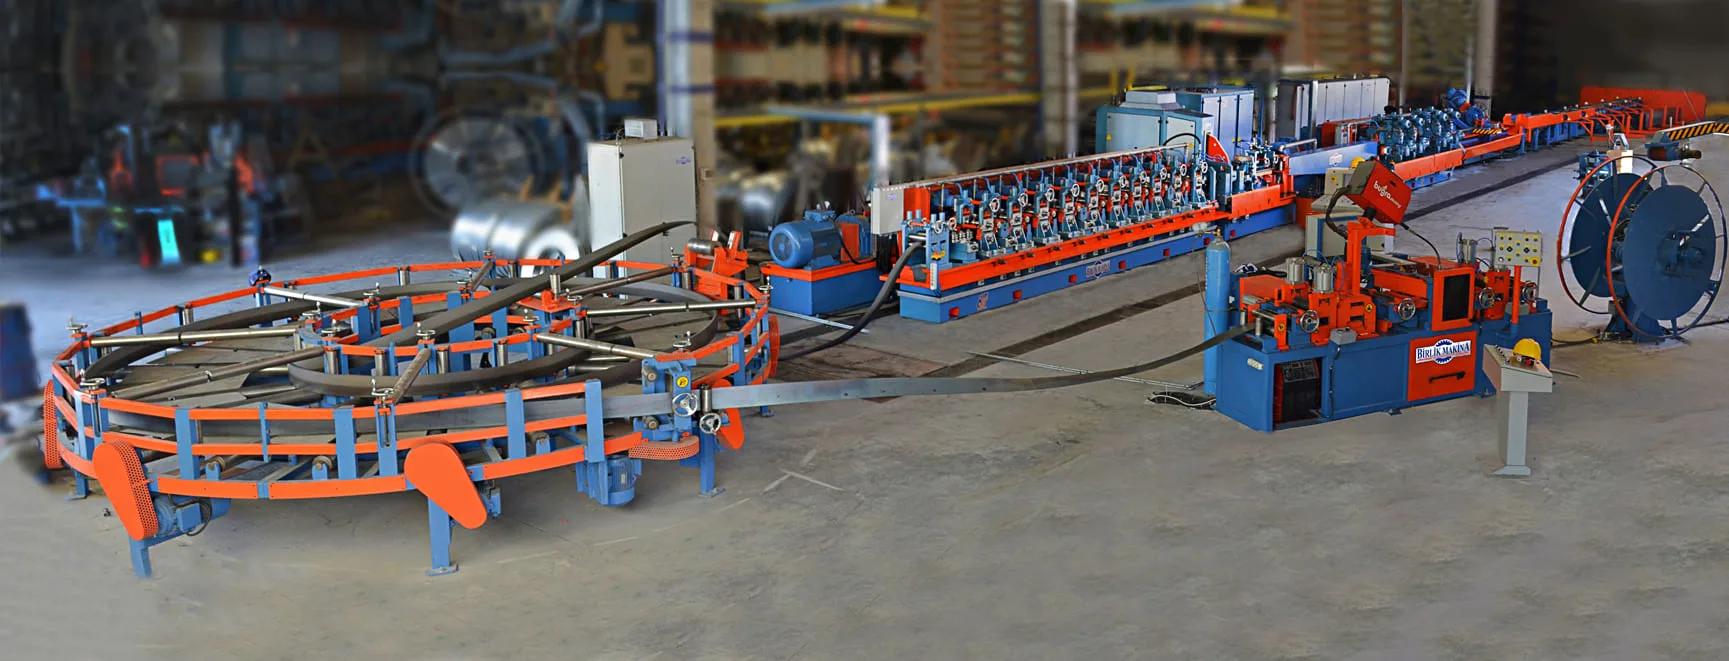
Birlik Makina engineers and builds turnkey high-frequency welded (ERW) tube and profile mills covering a wide range from Ø10 mm to Ø406 mm. Every group of the line — from the decoiler to the packing unit — together with its automation and roll tooling, is designed and manufactured in our own factory.
We have installed hundreds of lines in Türkiye and abroad. The BTM series below shows our standard models; we engineer your line around the diameter, wall thickness, speed and product length you need.
Fast size changes
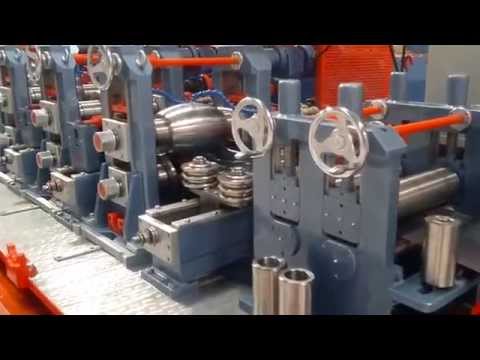
Thanks to the automatic roll adjustment system and quick-change options, switching from one product size to another takes less time — and your line spends more time producing.
Key features
- Ø10 – Ø406 mm tube, 10×10 – 300×300 mm square and rectangular profiles
- Automatic roll adjustment system and fast size changes
- Spiral accumulator for uninterrupted production
- Solid-state high-frequency welder
- Cold or hot flying saw cutting without stopping the line
- Automatic conveyor, kick-off and double-sided stacking table
- European automation and hydraulic components
- Installation, commissioning, training and a 1-year full warranty
BTM series technical specifications
Scroll sideways to see the full table| Model | Tube diameter (mm) | Square / rectangular profile (mm) | Tube wall thickness (mm) | Profile wall thickness (mm) | Max. speed (m/min) | Product length (mm) |
|---|---|---|---|---|---|---|
| BTM 100 | Ø10 – Ø32 | 10×10 – 25×25 | 0.50 – 1.50 | 0.50 – 1.20 | 160 | 3000 – 7500 |
| BTM 120 | Ø13 – Ø38 | 10×10 – 30×30 | 0.60 – 2.00 | 0.60 – 1.50 | 150 | 3000 – 7500 |
| BTM 160 | Ø16 – Ø51 | 15×15 – 40×40 | 0.70 – 2.50 | 0.70 – 2.00 | 140 | 3000 – 7500 |
| BTM 200 | Ø21 – Ø63 | 20×20 – 50×50 | 0.80 – 3.00 | 0.80 – 2.50 | 130 | 3500 – 8000 |
| BTM 240 | Ø25 – Ø76 | 20×20 – 60×60 | 0.80 – 3.50 | 0.80 – 3.00 | 120 | 3500 – 8000 |
| BTM 280 | Ø32 – Ø89 | 25×25 – 70×70 | 1.00 – 4.00 | 1.00 – 3.50 | 110 | 4000 – 8000 |
| BTM 320 | Ø38 – Ø102 | 30×30 – 80×80 | 1.20 – 6.00 | 1.20 – 5.00 | 100 | 5000 – 12000 |
| BTM 400 | Ø51 – Ø127 | 40×40 – 100×100 | 1.50 – 6.35 | 1.50 – 6.00 | 90 | 5000 – 12000 |
| BTM 525 | Ø89 – Ø168 | 70×70 – 120×120 | 2.00 – 7.00 | 2.00 – 6.00 | 80 | 5000 – 12000 |
| BTM 685 | Ø114 – Ø219 | 90×90 – 150×150 | 2.50 – 8.00 | 2.50 – 6.00 | 70 | 6000 – 12000 |
| BTM 860 | Ø140 – Ø274 | 110×110 – 200×200 | 3.00 – 10.00 | 3.00 – 8.00 | 60 | 6000 – 12000 |
| BTM 1000 | Ø168 – Ø327 | 130×130 – 250×250 | 3.00 – 10.00 | 3.00 – 8.00 | 50 | 6000 – 12000 |
| BTM 1275 | Ø219 – Ø406 | 150×150 – 300×300 | 4.00 – 12.70 | 4.00 – 10.00 | 40 | 6000 – 12000 |
* The machines listed are standard models; we engineer and build turnkey lines for the diameter, wall thickness and capacity you need.
** Speeds are given for S245 (St37) material at 6 m length.
Line layout
Explore the line from start to finish
Drag the plan, zoom in or tap a station. Units with photos open in detail with a single tap.

01
Uncoiler
02
Coil opener and leveller
03
Automatic shear welder
04
Rotator
05
Accumulator
06
Forming entry section
07
Forming section
08
Welding section
09
Scarfing section
10
Cooling tunnel
11
Sizing section
12
Turk’s head
13
Flying saw
14
Conveyor and packing
Whole line
ERW Tube and Profile Mills
Our tube and profile mill consists of the following units
- Hydraulic coil car
- Decoiler (hydraulic)
- 7-roll straightener
- Strip end welder (automatic as an option)
- Accumulator
- Leveller group
- Forming section
- Guide section
- Welding section
- High-frequency welder
- Cooling tower and pump
- Deburring unit (automatic)
- Cooling tunnel
- Sizing section
- Weld testing unit
- Turk’s head
- Saw unit (cold or hot cutting)
- Conveyor and kick-off unit (automatic)
- Double-sided stacking table
- Drive unit
- Electrical group
- Hydraulic group
- Complete roll tooling
- Spare parts
- Installation and commissioning
- 1-year full warranty
ERW Tube and Profile Mills
Line units
Tap a card for details on each unit.
01 / 11
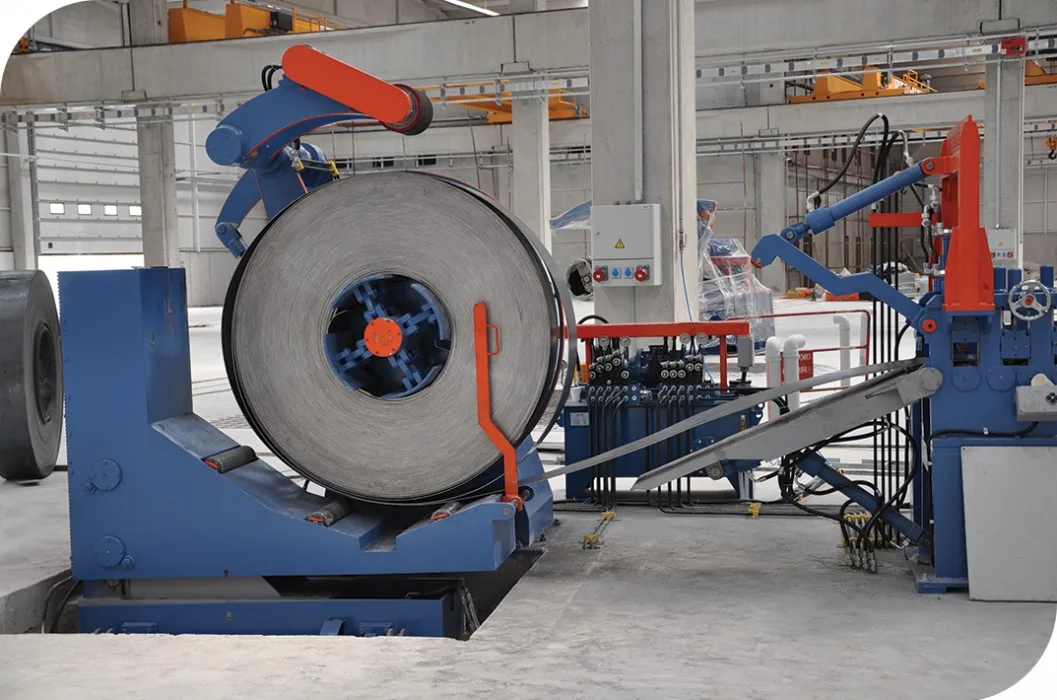
Decoiler
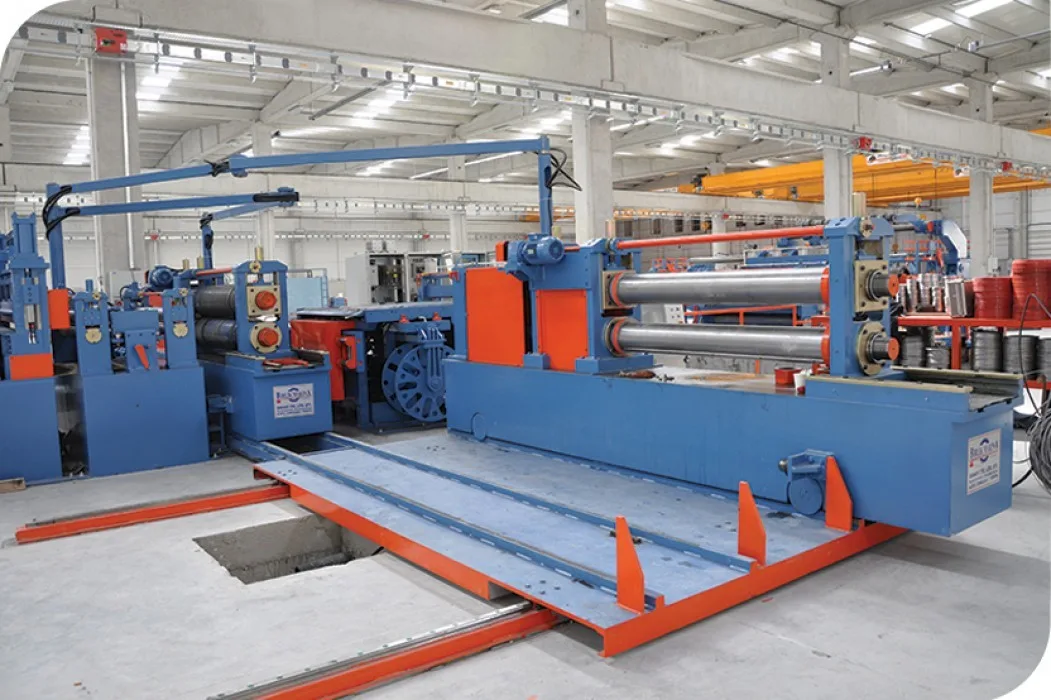
The first unit, feeding the line. Built with a single or double mandrel. On double-mandrel types the rotation is set automatically: while one mandrel feeds the line, a new slit coil can be loaded on the other. Coil loading, brake and hold-down roll settings are controlled by the operator.
02 / 11
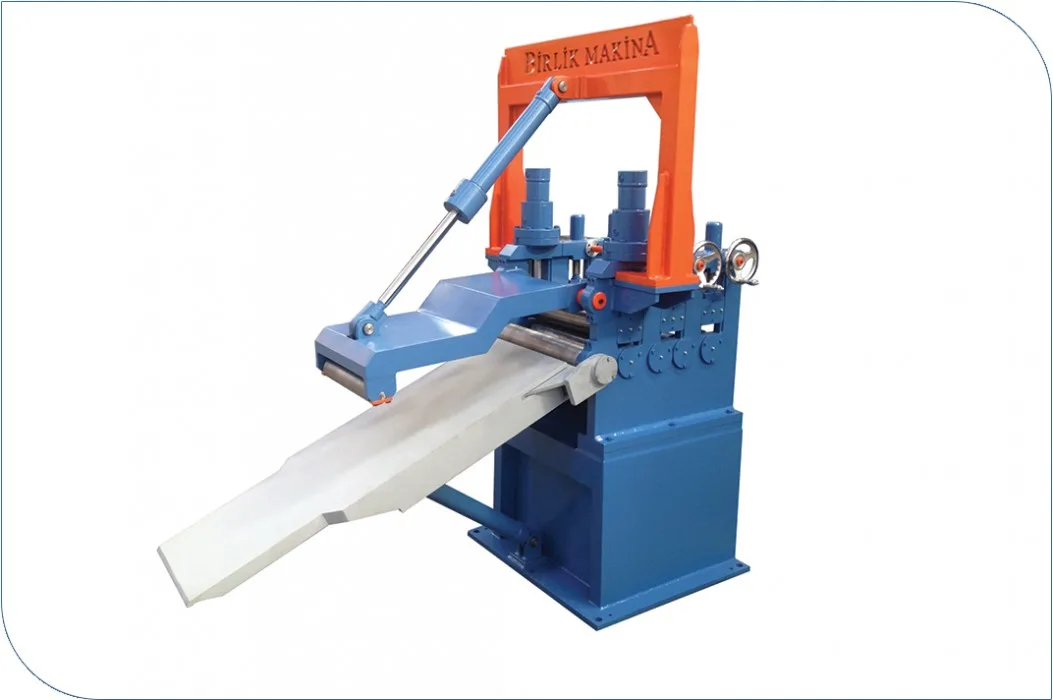
Decoiler and Straightening Unit
Corrects the leading end of the strip coming from the decoiler and guides it safely to the straightening unit, ensuring a clean entry into the line.
03 / 11
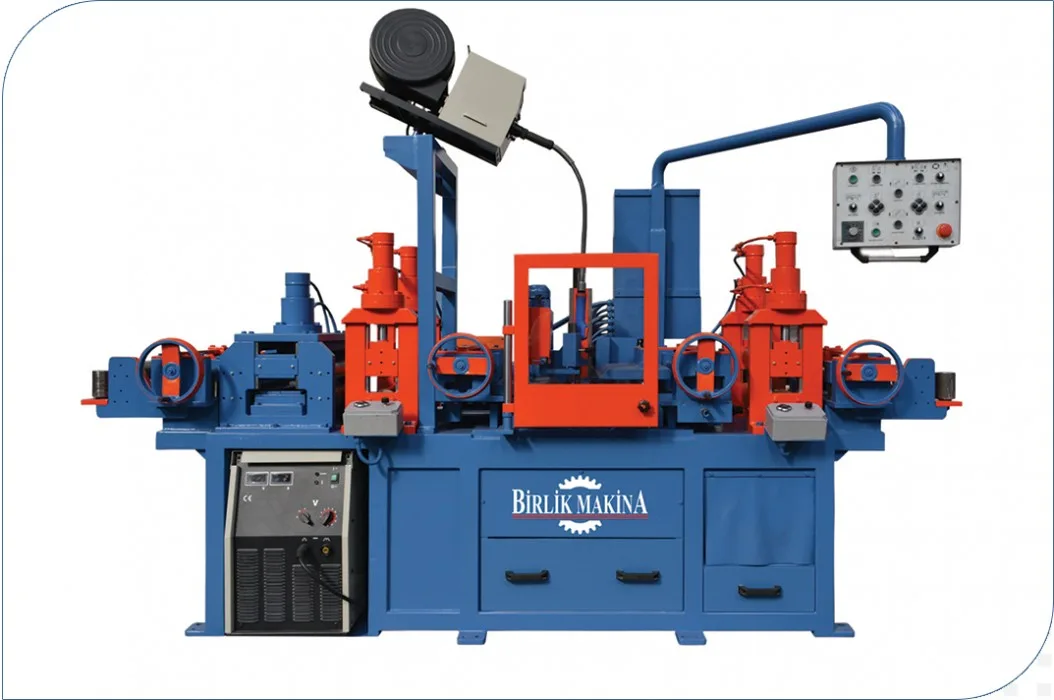
Semi-Automatic Strip End Welder
Joins the tail of the finished coil to the head of the new coil so the line can run without interruption. Shearing, joining and clamping are automatic; the end weld is completed by MIG welding.
04 / 11
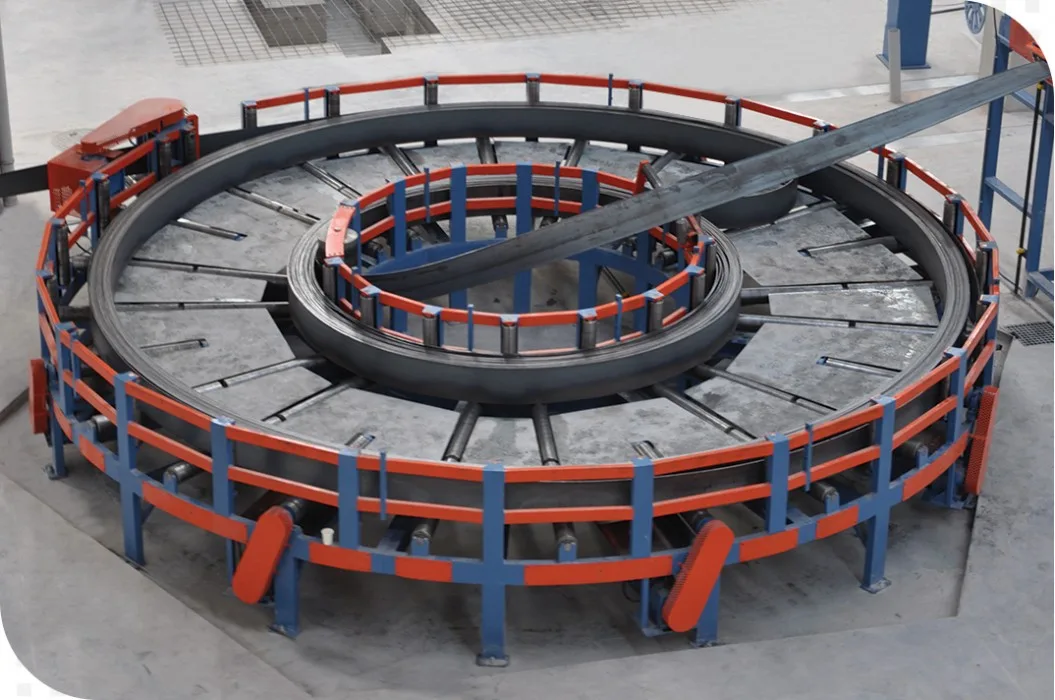
Accumulator
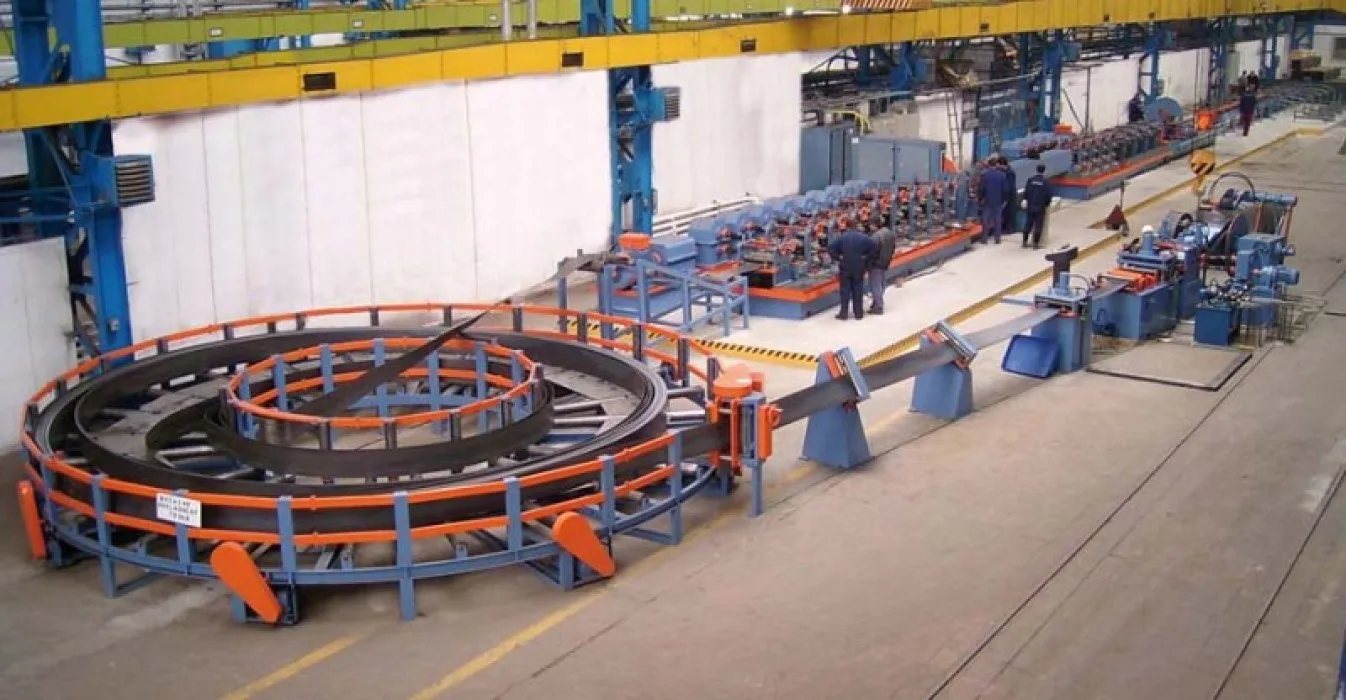
Stores strip so that the line does not stop while the strip ends are being welded. The spiral accumulator lets the tube and profile mill run continuously.
05 / 11
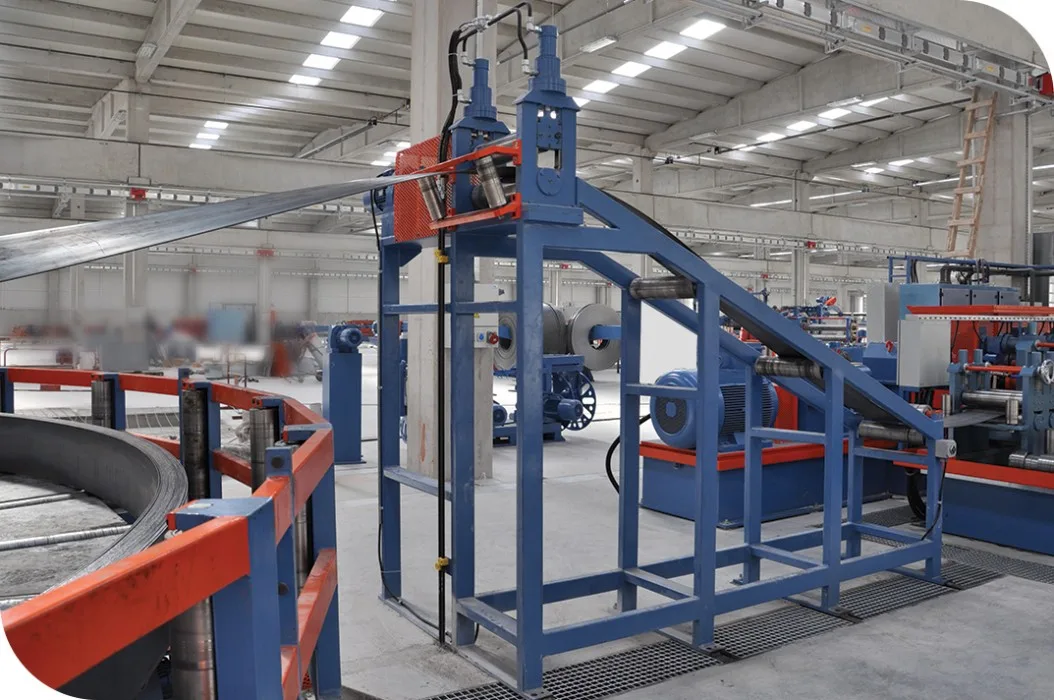
Forming Entry Section
Aligns the strip coming from the spiral accumulator and feeds it into the forming section of the mill in a controlled way.
06 / 11
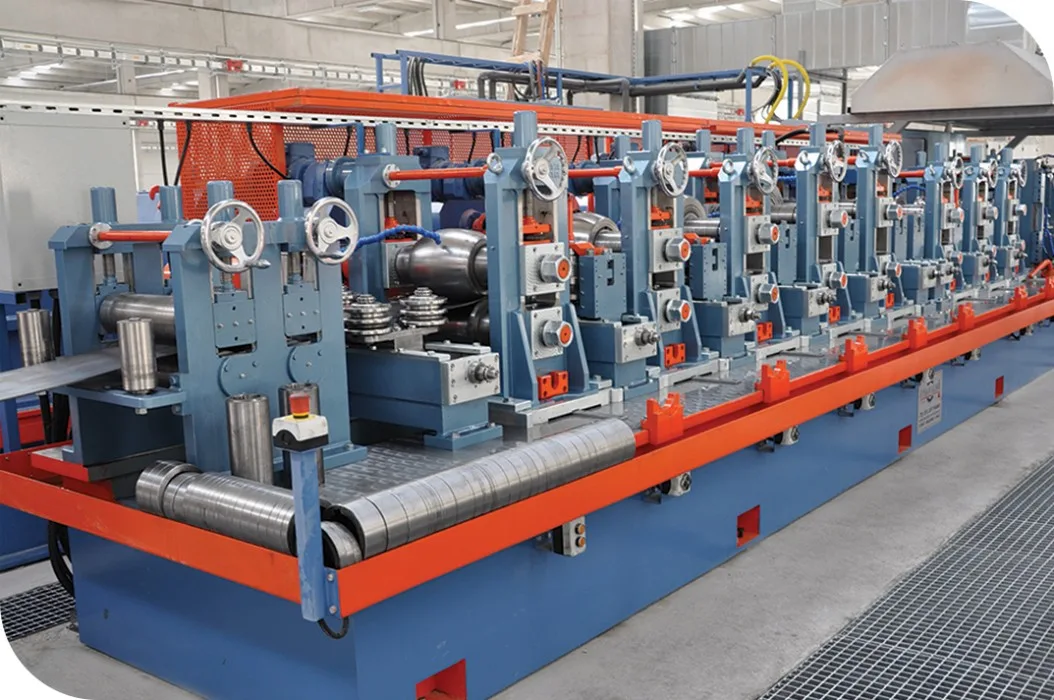
Forming Section
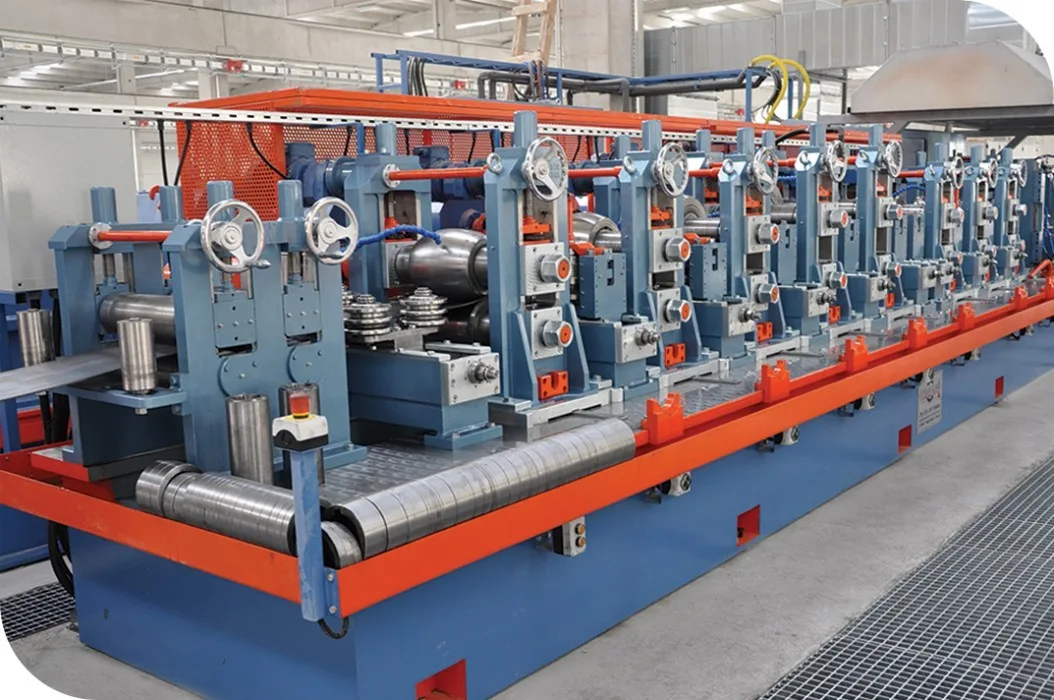
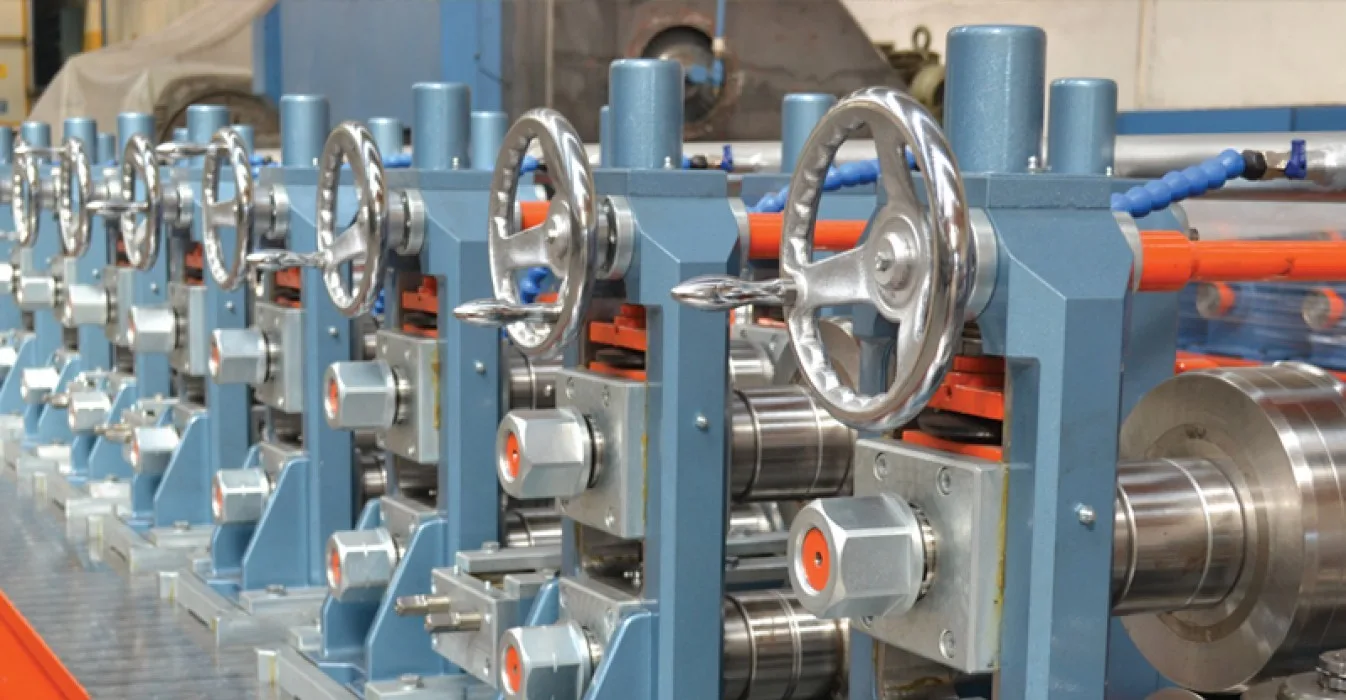
The section where the strip is given its initial tube shape. It consists of 7 vertical stands, 7 side stands, gearboxes, the main drive motor and cardan shafts.
07 / 11
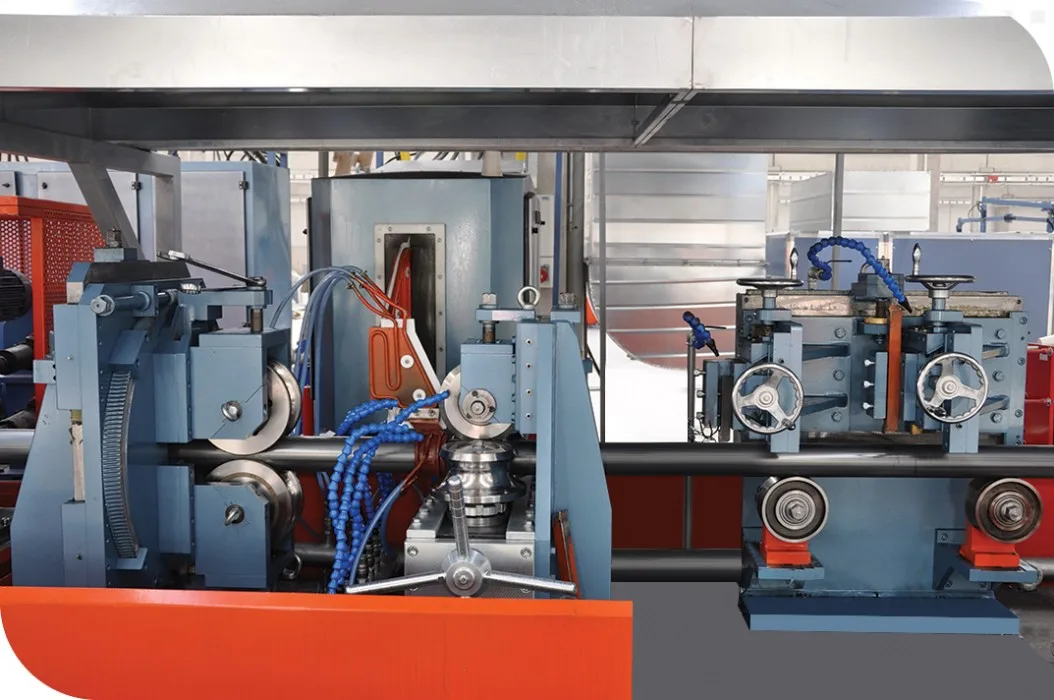
Welding and Deburring Section
The edges of the strip coming from the guide rolls are heated by the high-frequency welder and pressed together by three-roll squeeze stands. Once welded, the outside weld bead is removed in the same section.
08 / 11
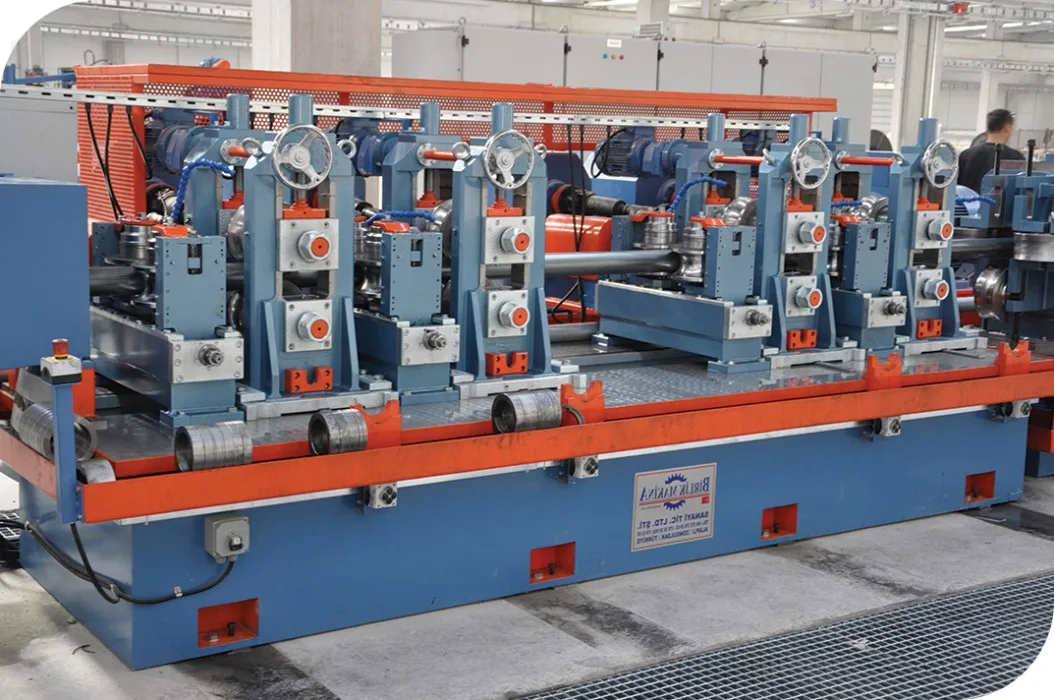
Sizing Section
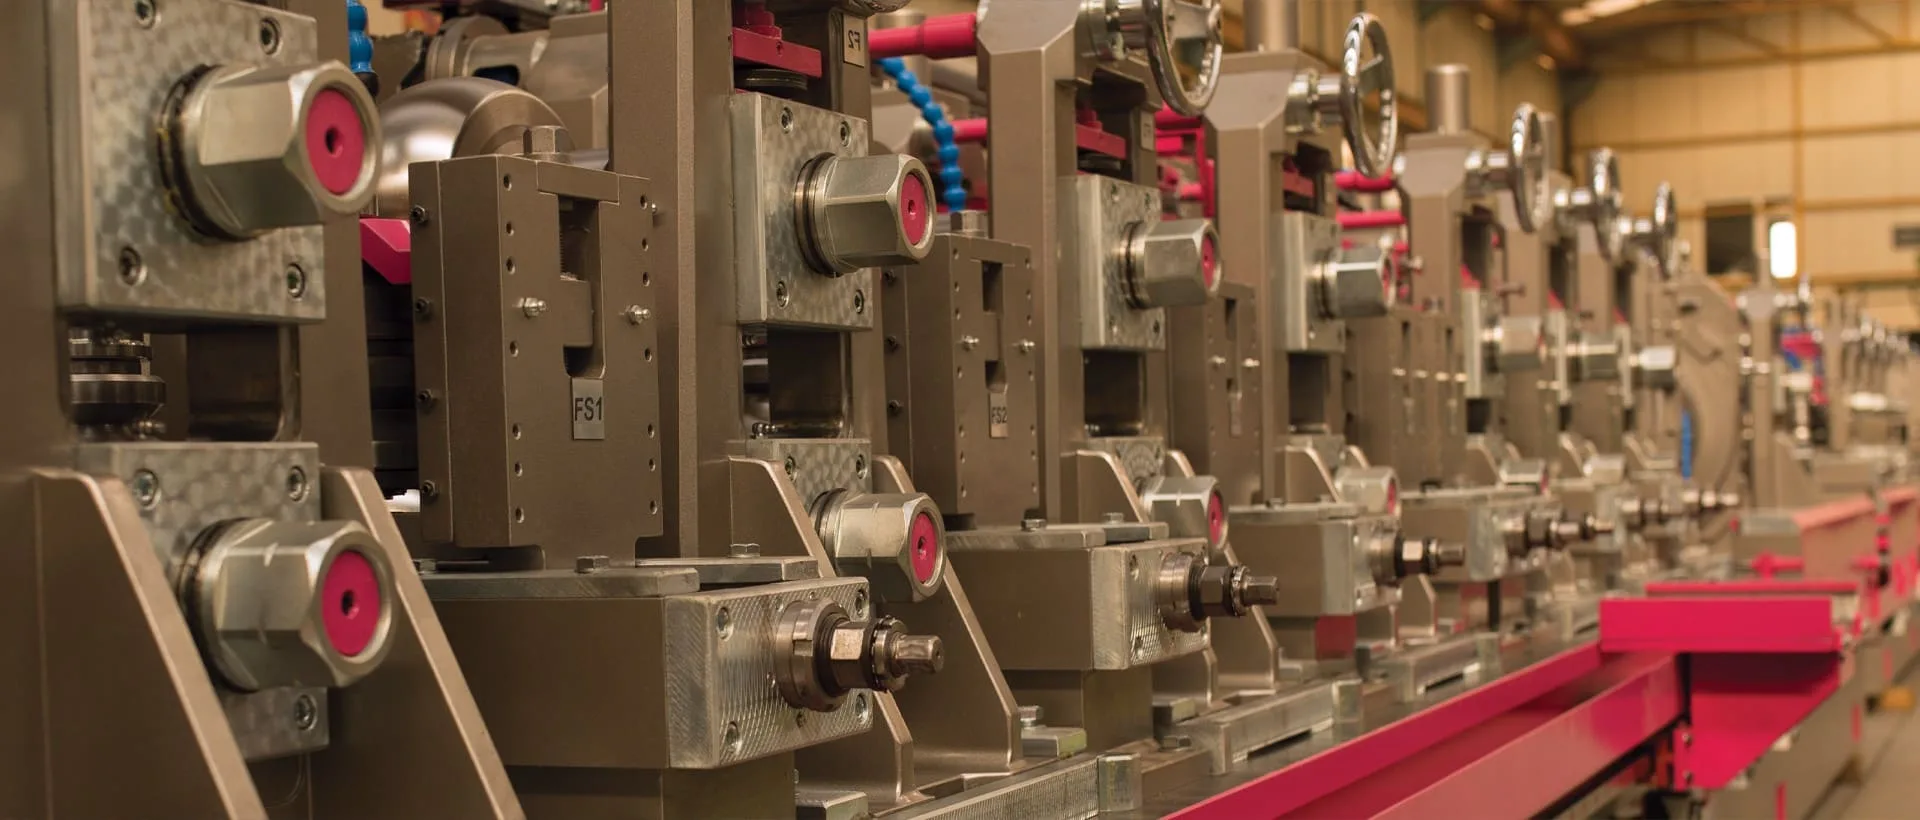
The section where the tube is brought to its final diameter. It consists of 4 vertical stands, 4 side stands, gearboxes, the main drive motor and cardan shafts.
09 / 11
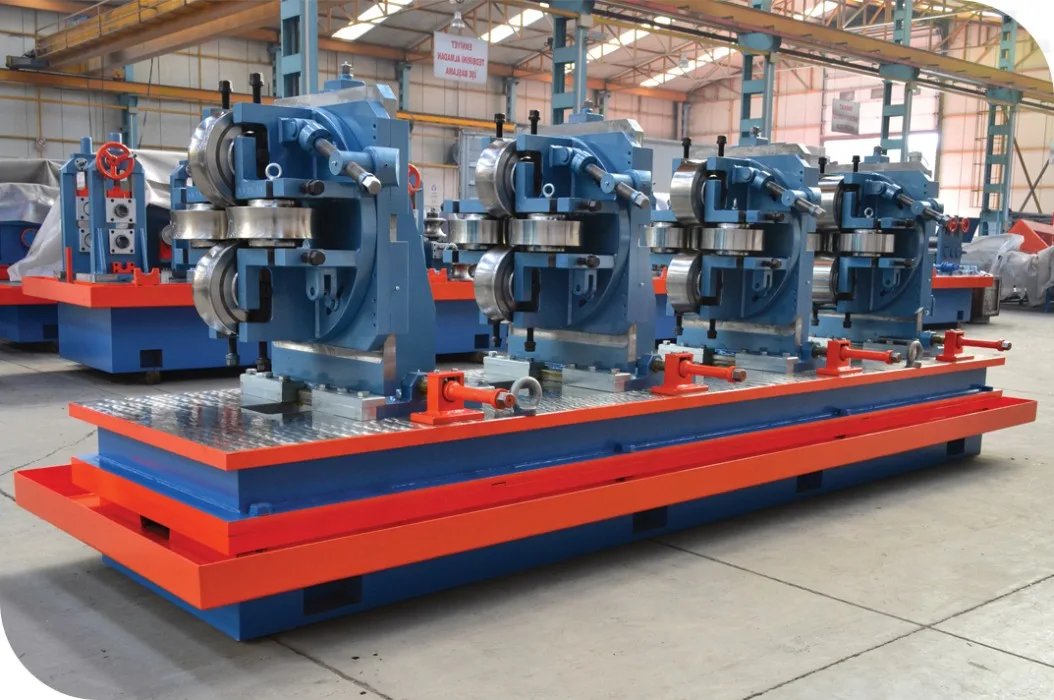
Turk’s Head Section
The tube, now at its final diameter, is turned into a square or rectangular profile by rolls. Straightness of the tube or profile is also corrected here.
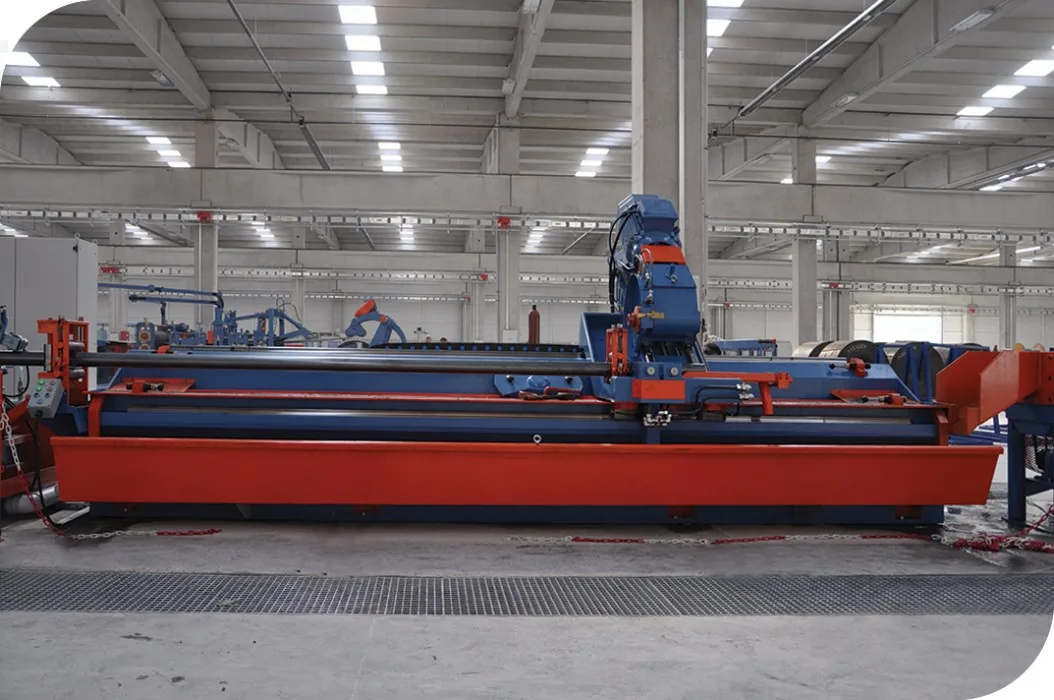
10 / 11
Flying Cold Saw
Cuts the finished tube or profile to the required length without stopping the line. It travels on a linear slide mounted on the frame and performs all its functions automatically, synchronised with the tube mill.
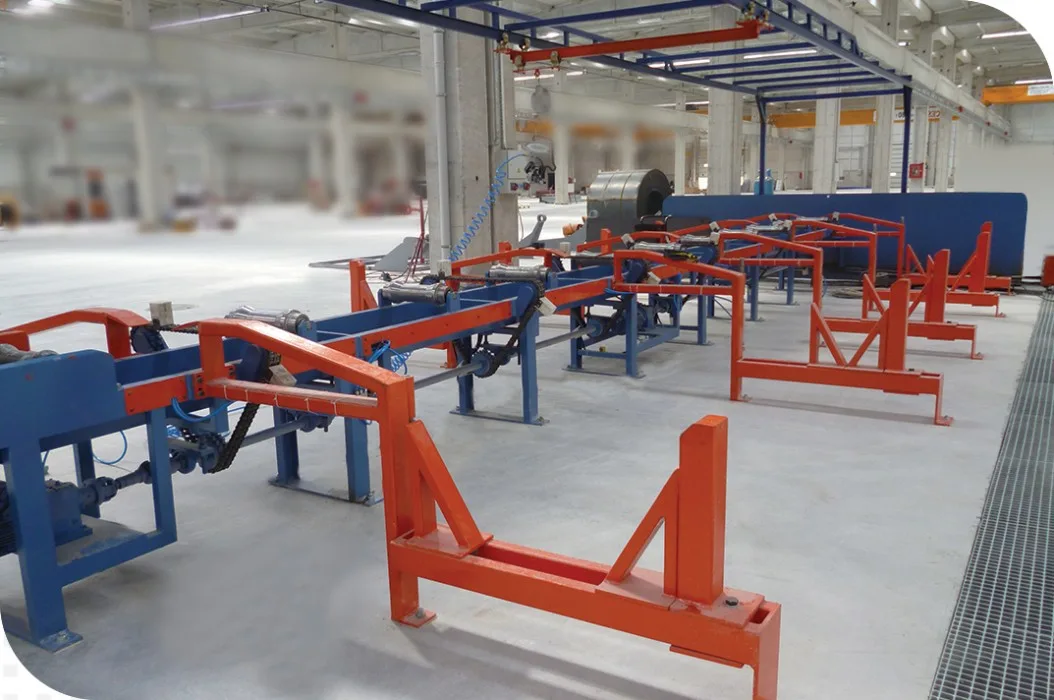
11 / 11
Conveyor and Packing Section
Tubes and profiles cut by the saw are carried by conveyor to the kick-off unit, which drops them onto the stacking table. Tubes can be packed in hexagonal bundles and profiles in square bundles on both sides.
ERW Tube and Profile Mills
Videos
BTM 240 tube mill (Ø21 – Ø63 mm)
Tube mills
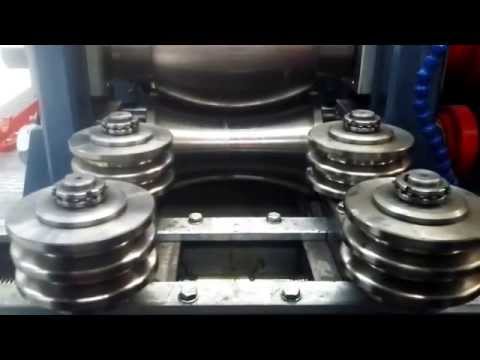
Automatic roll adjustment system
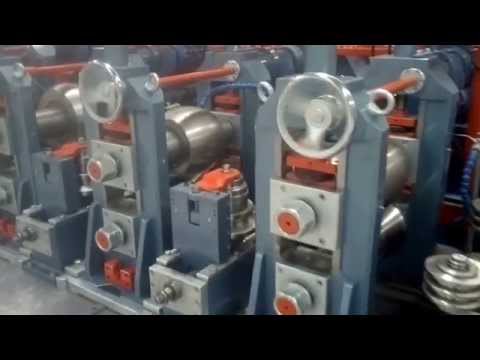
Automatic roll adjustment system — in operation
The video loads from YouTube when you press play.
ERW Tube and Profile Mills
Gallery
ERW Tube and Profile Mills
Frequently asked questions
Share your material, product dimensions and capacity target — our engineers will prepare a technical proposal tailored to you.
Which tube and profile sizes can I produce?
The standard BTM series covers Ø10 – Ø406 mm tube and 10×10 – 300×300 mm square and rectangular profiles, with wall thicknesses of 0.50 – 12.70 mm. For sizes outside this range we engineer the line around your needs.
Is the line delivered turnkey?
Yes. Design, manufacturing, installation, commissioning and operator training are carried out by our own teams. Complete roll tooling and spare parts are included in the scope of supply.
Under which conditions do the speeds in the table apply?
Speeds are given for S245 (St37) material at 6 m length. Actual speed depends on material grade, wall thickness and cut length.
What warranty and after-sales support do you provide?
We give a 1-year full warranty covering both mechanical and automation systems, and provide spare parts and technical service to customers worldwide.
Production lines
Other production lines
02
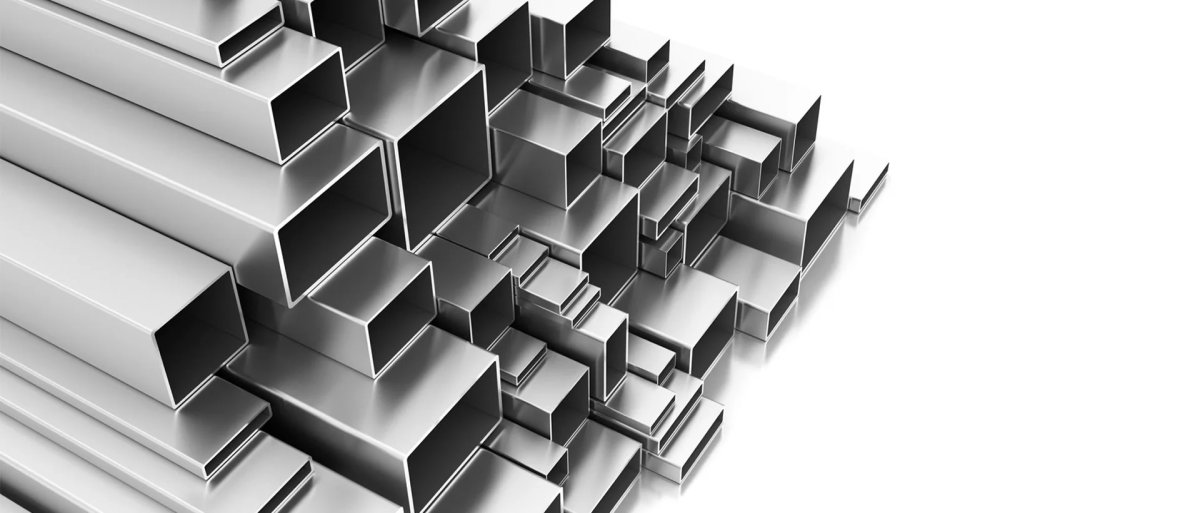
Direct Forming Tube Mills
Direct forming lines that produce 20×20 – 120×120 mm square and rectangular profiles with no roll change — sizes are set from the computer.
- Profile size
- 20×20 – 120×120 mm
- Wall thickness
- 1.10 – 6.00 mm
- Line speed
- up to 130 m/min
03
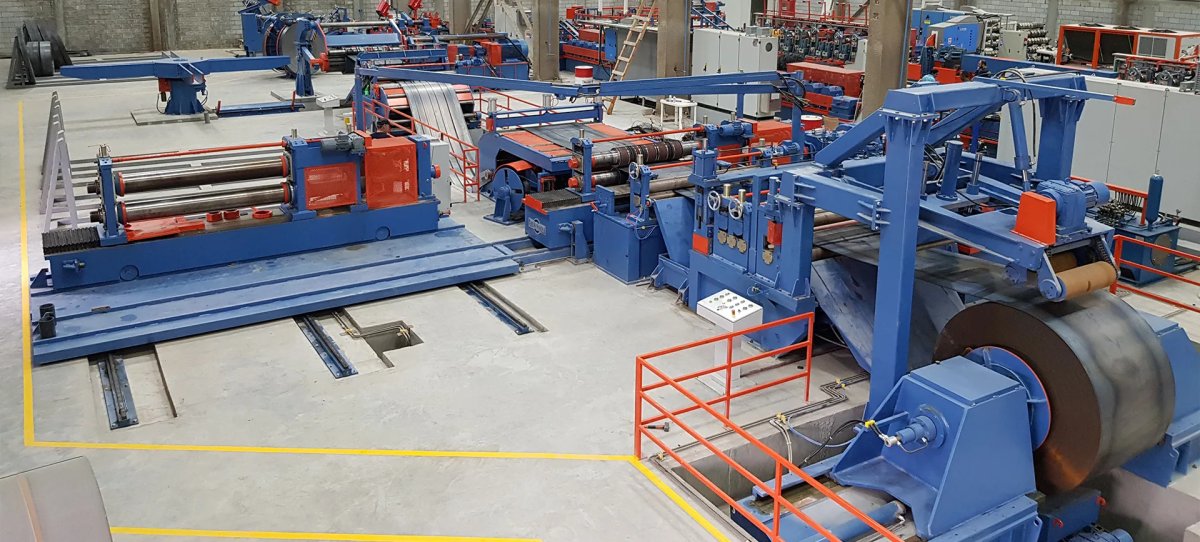
Coil Slitting Lines
Slitting lines with optional double slitter head that cut 0.50 – 12.00 mm coils up to 2000 mm wide into strips of the required width.
- Sheet thickness
- 0.50 – 12.00 mm
- Coil width
- up to 2000 mm
- Coil weight
- up to 30 t
04
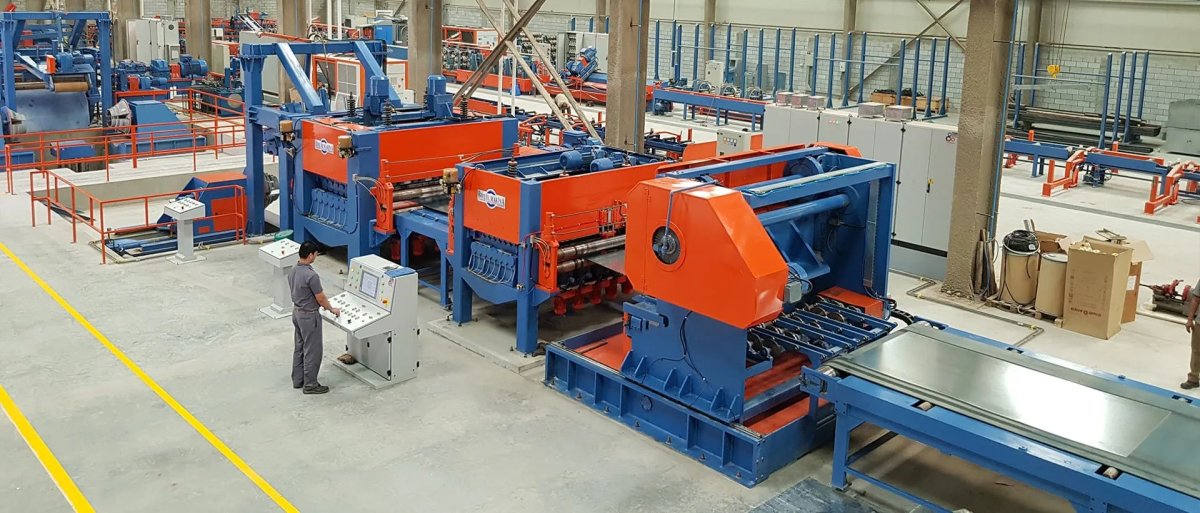
Cut-to-Length Lines
Cut-to-length lines that level 0.50 – 16.00 mm coils, cut them to the required length without stopping, and stack the sheets automatically.
- Sheet thickness
- 0.50 – 16.00 mm
- Coil width
- up to 2000 mm
- Coil weight
- up to 30 t