Coil Slitting Lines
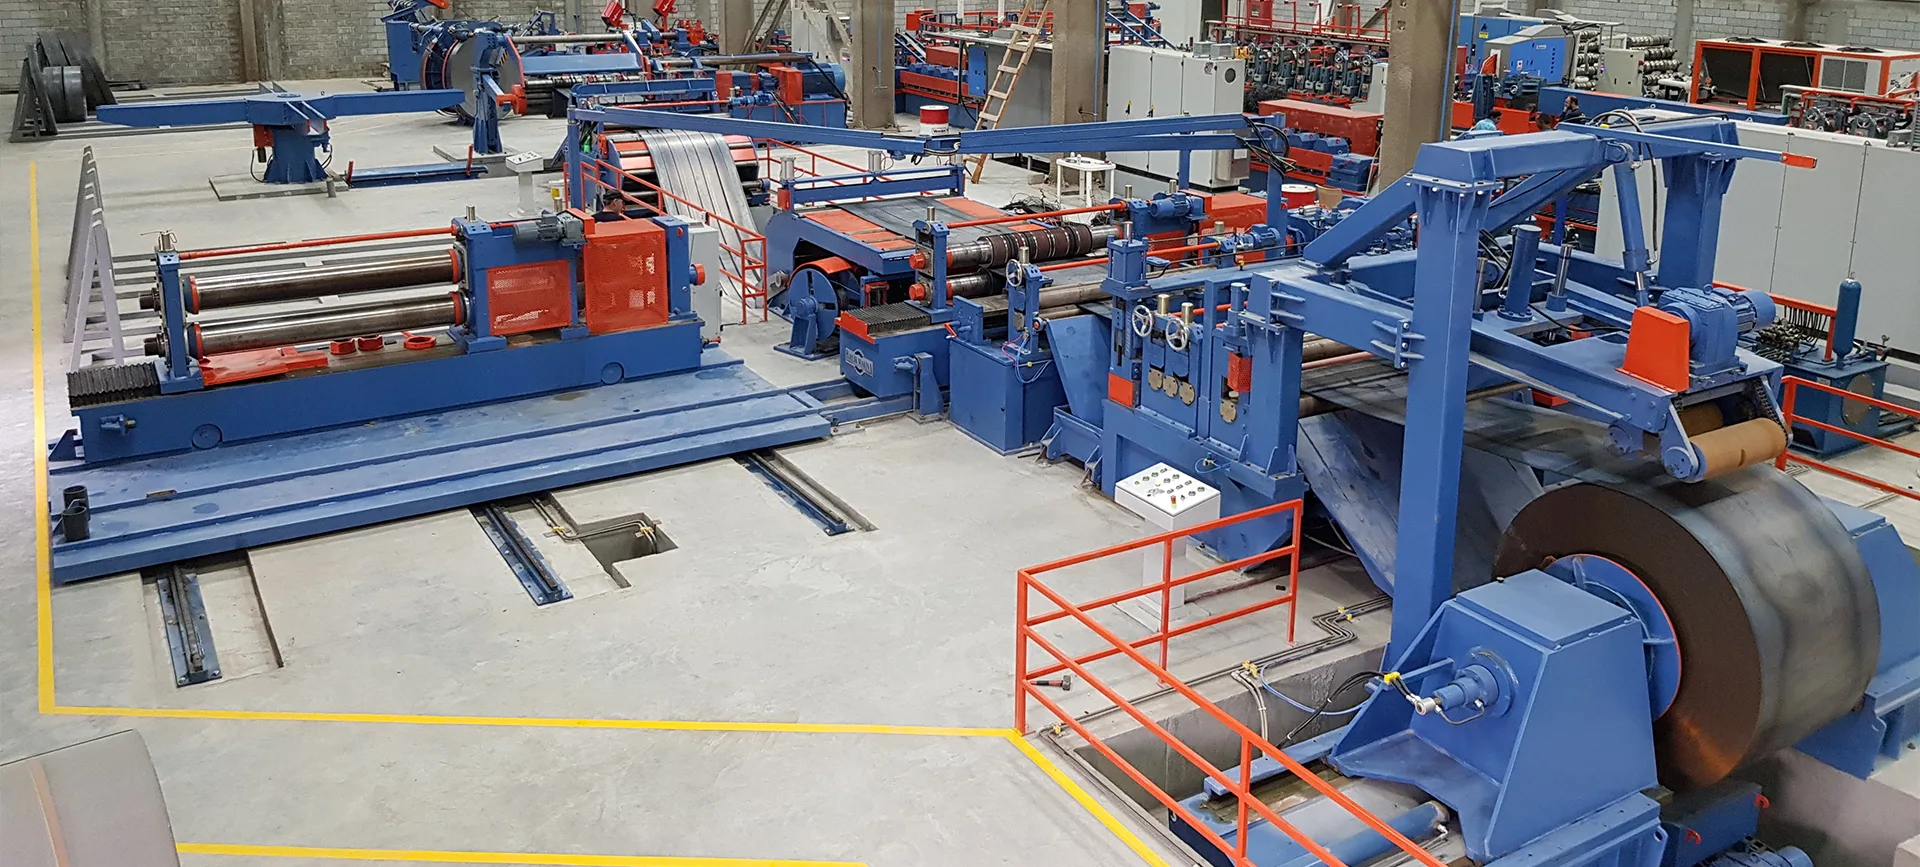
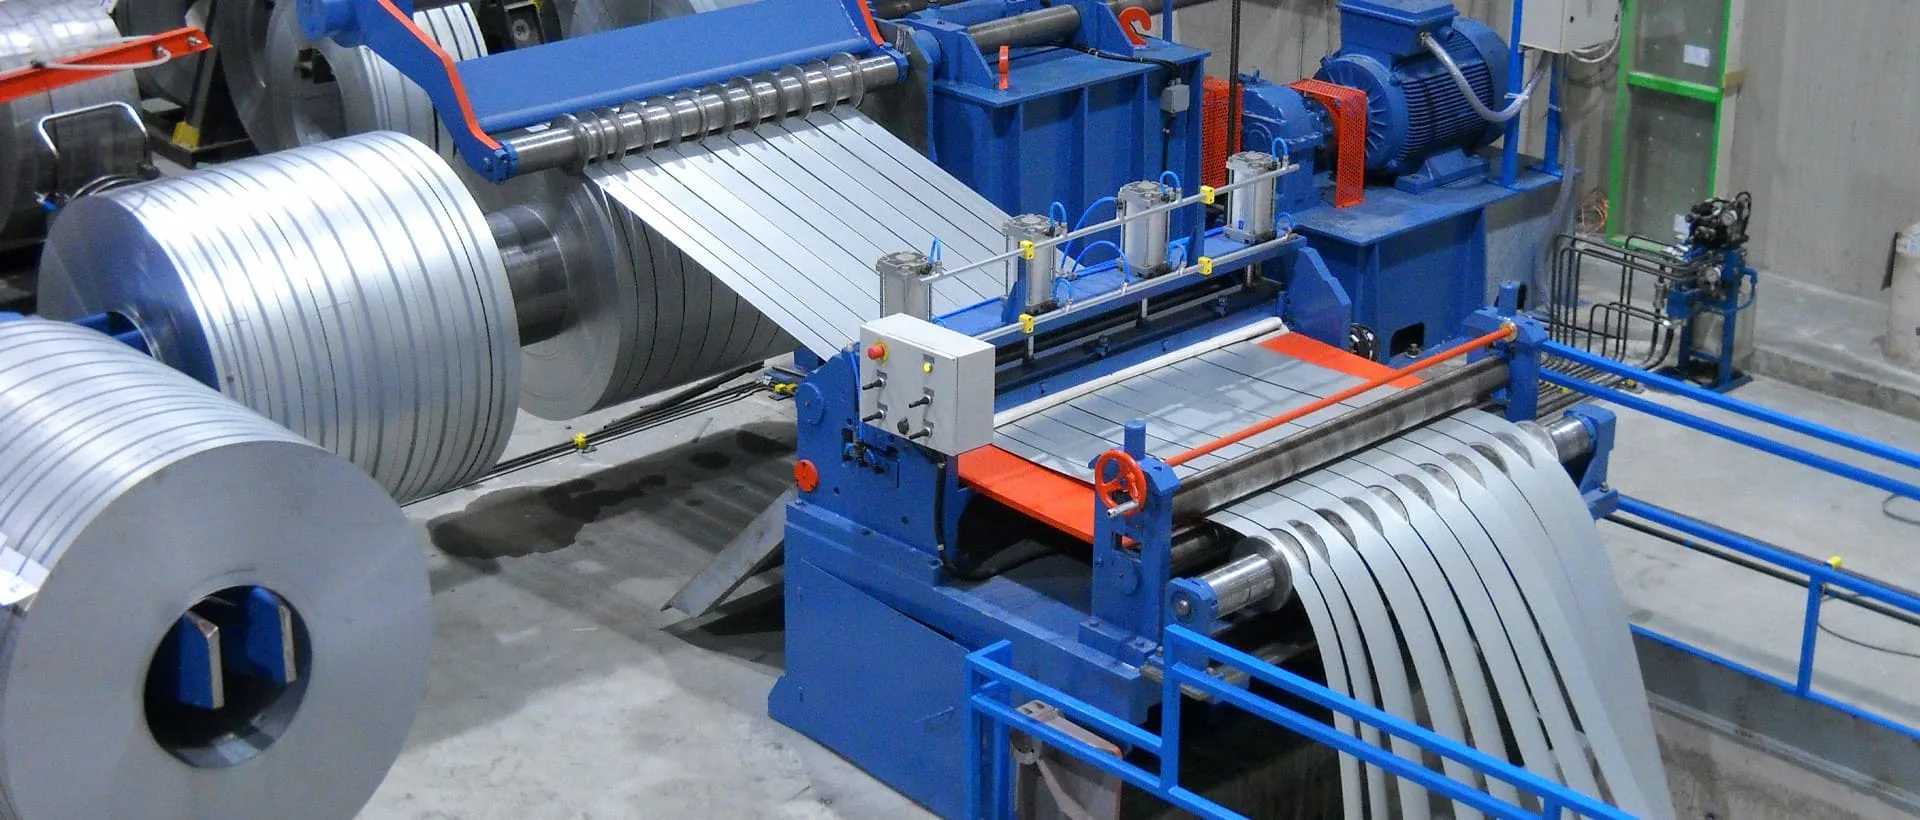
Slitting lines with optional double slitter head that cut 0.50 – 12.00 mm coils up to 2000 mm wide into strips of the required width.
- Sheet thickness
- 0.50 – 12.00 mm
- Coil width
- up to 2000 mm
- Coil weight
- up to 30 t
- Line speed
- up to 220 m/min
Overview
Birlik Makina engineers and builds turnkey coil slitting lines for thicknesses from 0.50 mm to 12.00 mm. Our lines meet the strip requirements of tube and profile producers, steel service centres and sheet-processing industries with high speed and precision.
An optional second slitter head, automatic coil tilting and fast knife changes reduce downtime and increase capacity. The models below are standard; we design the line that fits your needs together with you.
Key features
- Optional second (double) slitter head
- Automatic coil tilting system
- Fast knife change
- High production capacity
- 7-roll leveller and edge control unit
- Two independent scrap winders
- Loop pit and separator discs for tight, even recoiling
- Installation, training, tests and a 1-year full warranty
Coil slitting lines technical specifications
Scroll sideways to see the full table| Model | Sheet thickness (mm) | Coil width (mm) | Coil inner diameter (mm) | Coil outer diameter, max. (mm) | Coil weight, max. (t) | Strip coil inner diameter (mm) | Max. speed (m/min) |
|---|---|---|---|---|---|---|---|
| BSL 2.00 | 0.50 – 2.00 | 500 – 1600 | 508 – 610 | 1600 | 16 | 508 | 220 |
| BSL 3.00 | 0.80 – 3.00 | 500 – 1600 | 508 – 610 | 1800 | 18 | 508 | 180 |
| BSL 4.00 | 1.00 – 4.00 | 700 – 1600 | 508 – 800 | 2000 | 20 | 508 | 150 |
| BSL 6.00 | 1.50 – 6.00 | 800 – 1600 | 508 – 900 | 2200 | 25 | 508 | 120 |
| BSL 8.00 | 2.00 – 8.00 | 800 – 2000 | 610 – 900 | 2200 | 30 | 610 | 55 – 100 |
| BSL 10.00 | 3.00 – 10.00 | 900 – 2000 | 610 – 900 | 2200 | 30 | 610 | 50 – 90 |
| BSL 12.00 | 4.00 – 12.00 | 900 – 2000 | 610 – 900 | 2200 | 30 | 610 | 40 – 75 |
* The machines listed are standard models; we engineer lines for the thickness, width and capacity you need.
Line layout
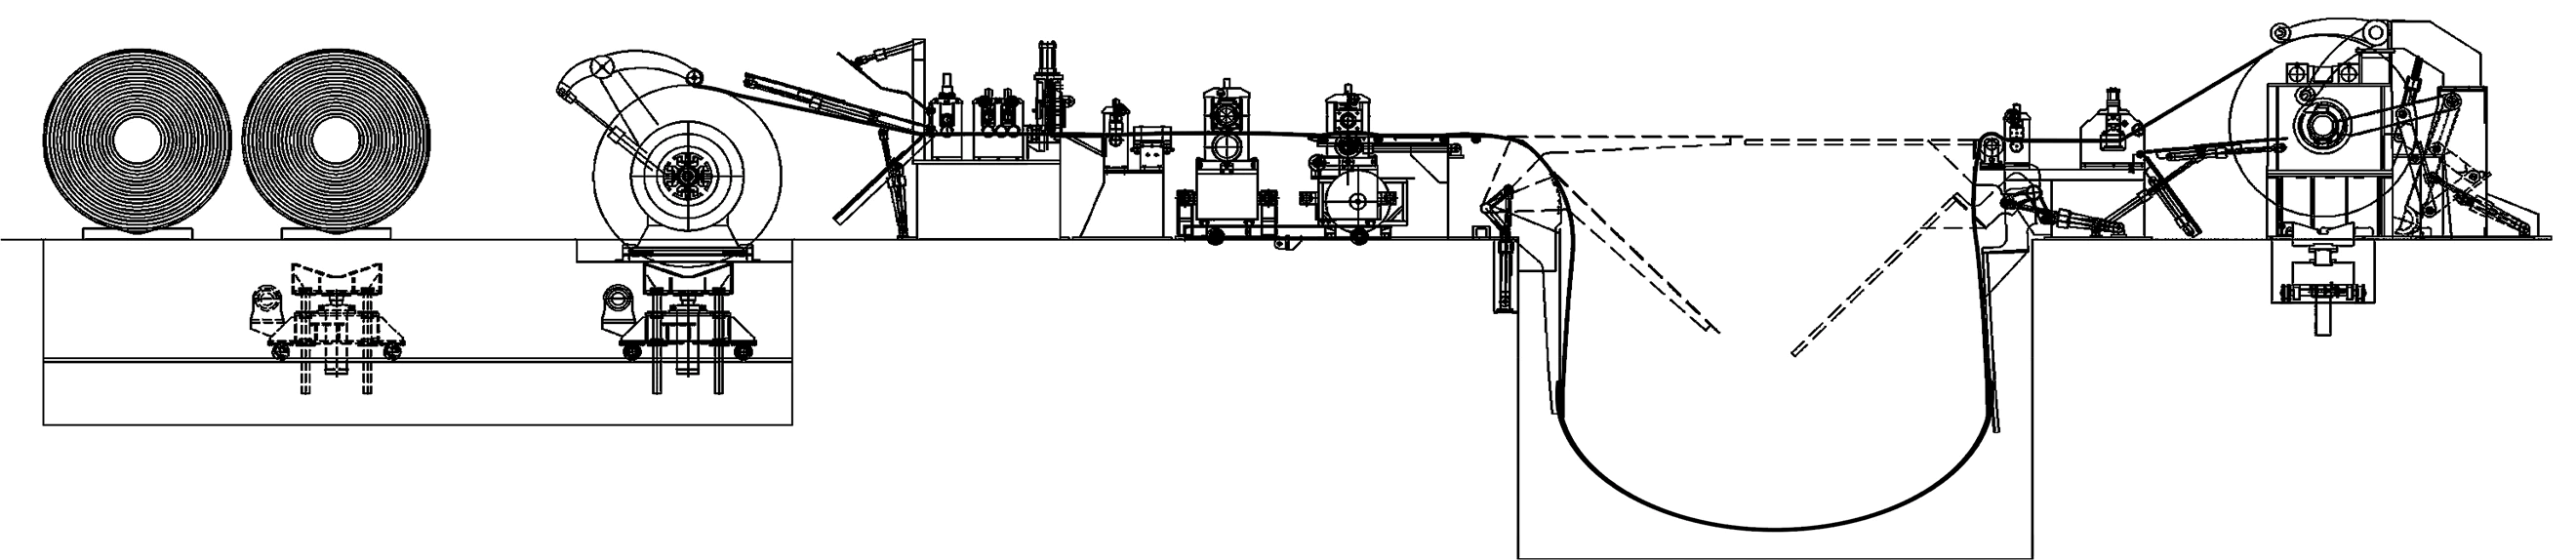
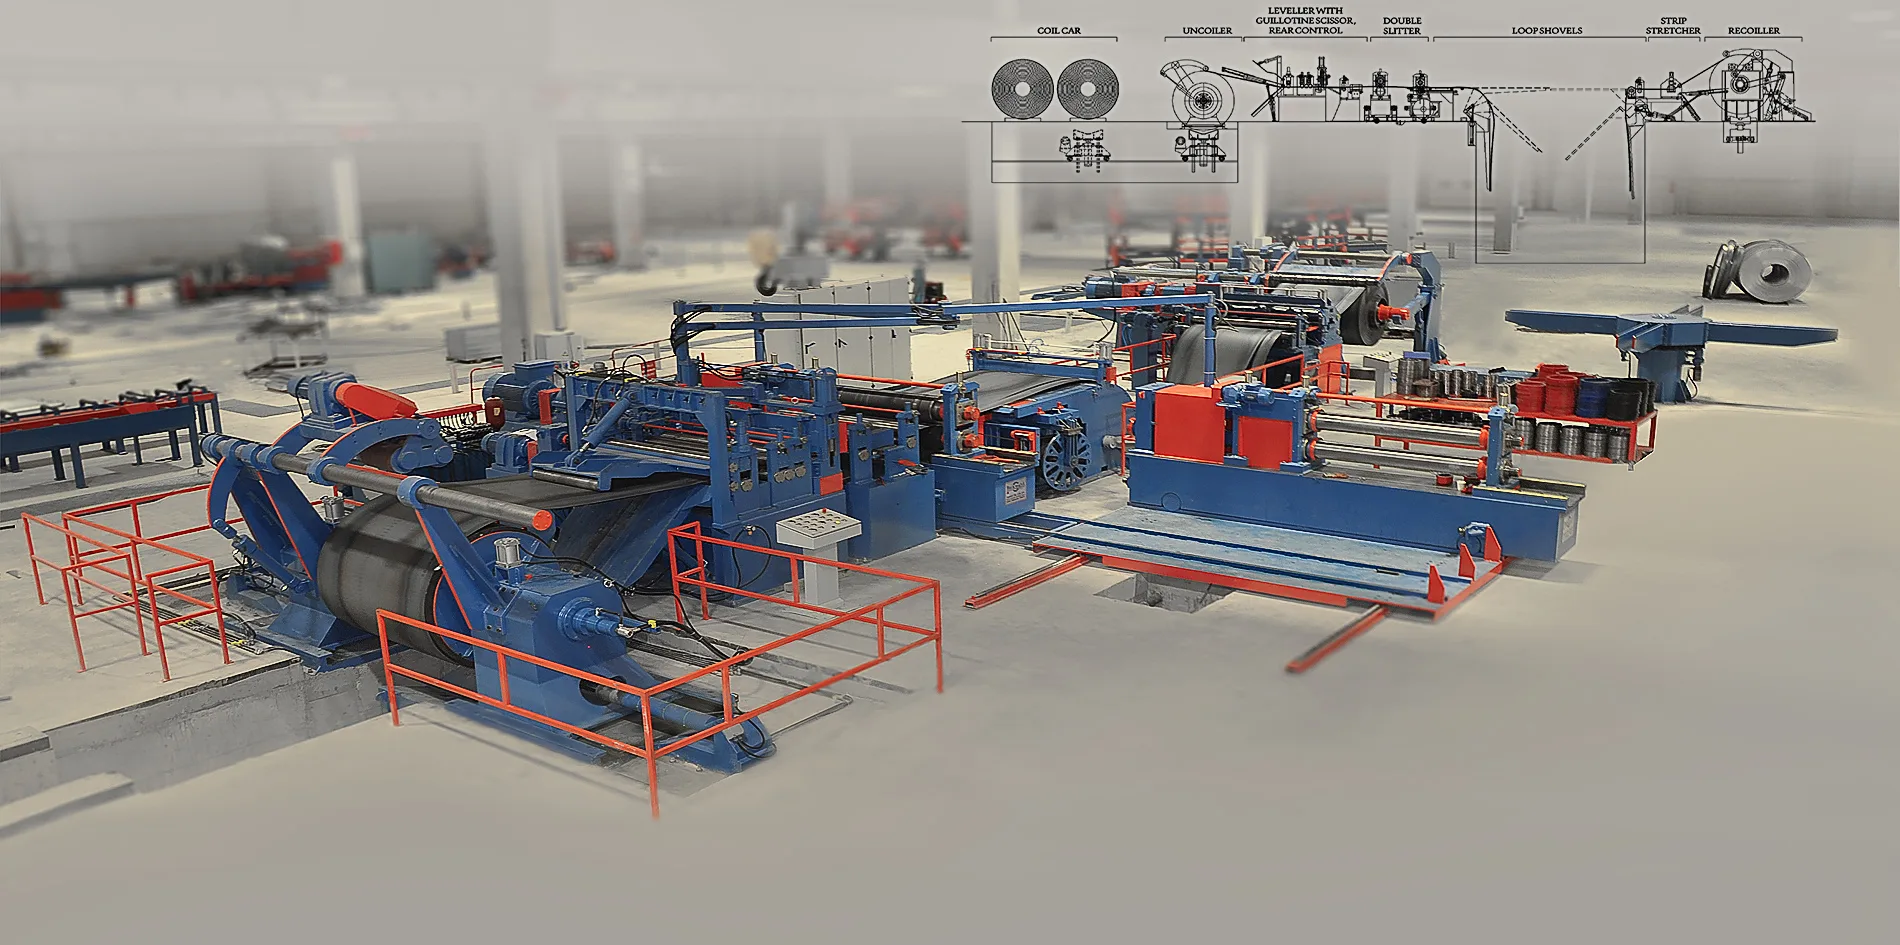
Explore the line from start to finish
Drag the plan, zoom in or tap a station. Units with photos open in detail with a single tap.
01
Coil car
02
Uncoiler
03
Leveller, guillotine shear and edge control
04
Double slitter
05
Loop pit
06
Strip tensioner
07
Recoiler
Whole line
Coil Slitting Lines
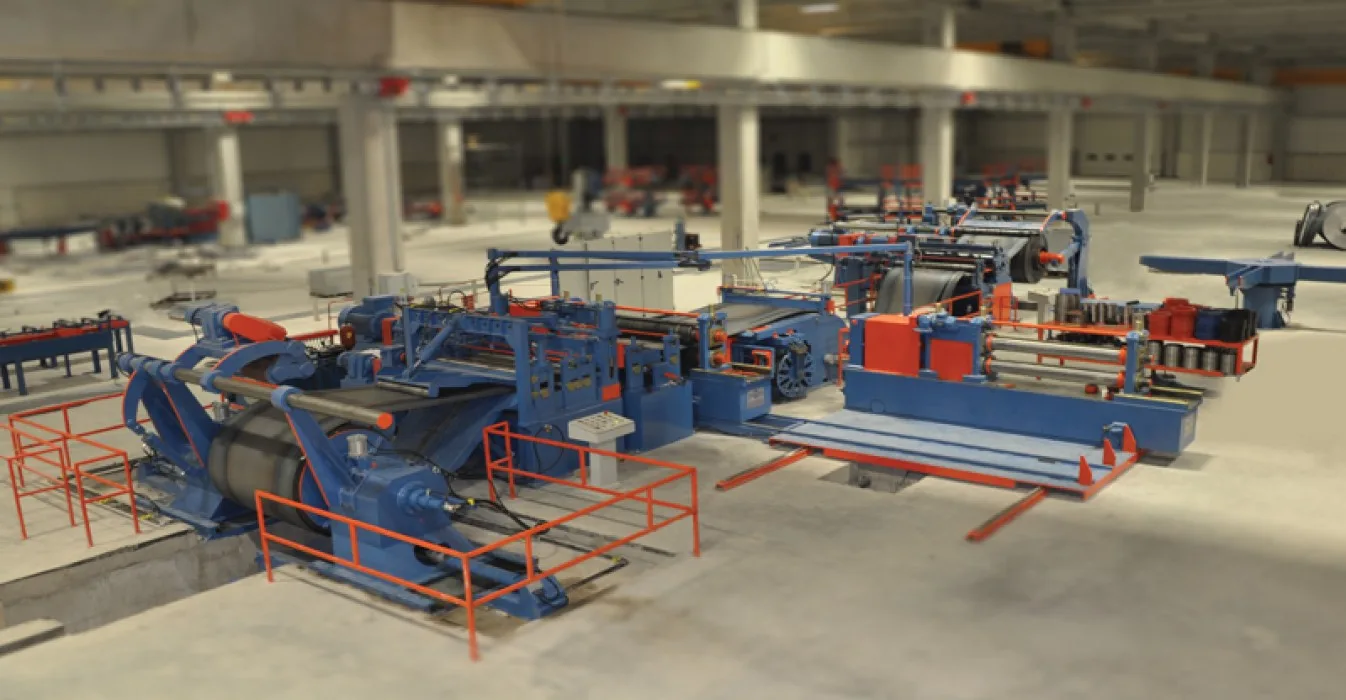
Our slitting line consists of the following units
- Coil car
- Decoiler
- 7-roll leveller
- Hydraulic shear
- Slitter unit
- Scrap winder
- Entry table
- Loop table
- Strip tensioning unit
- Recoiler
- Leveller drive group
- Hydraulic unit
- Slitter drive group
- Automation panel
- Control panel
- Separator
- Recoiler drive group
- Strip transfer unit
- Exit coil car
- Installation
- Spare parts
- Training and acceptance tests
- 1-year full warranty
Coil Slitting Lines
Line units
Tap a card for details on each unit.
01 / 09
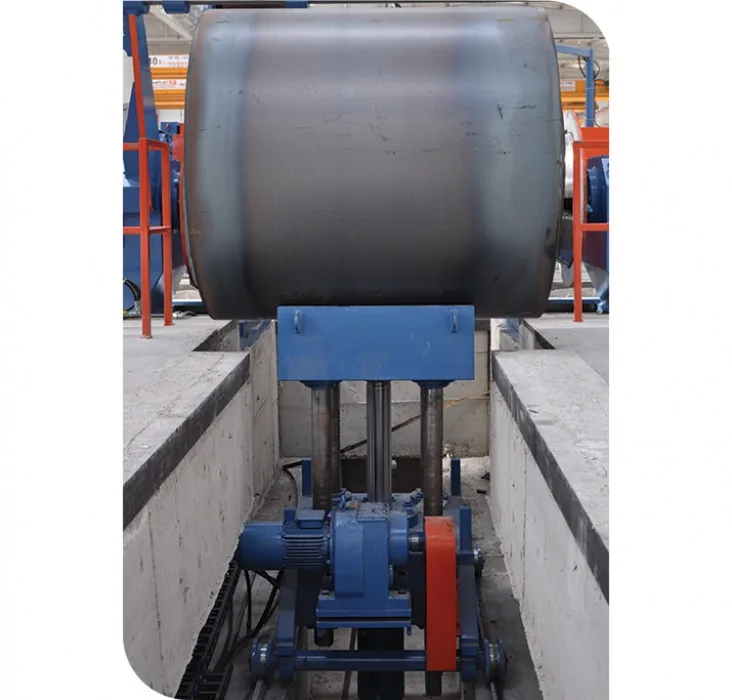
Coil Car
The unit where the coil to be slit first enters the line. The coil placed on the car is loaded onto the decoiler mandrel by this unit.
02 / 09
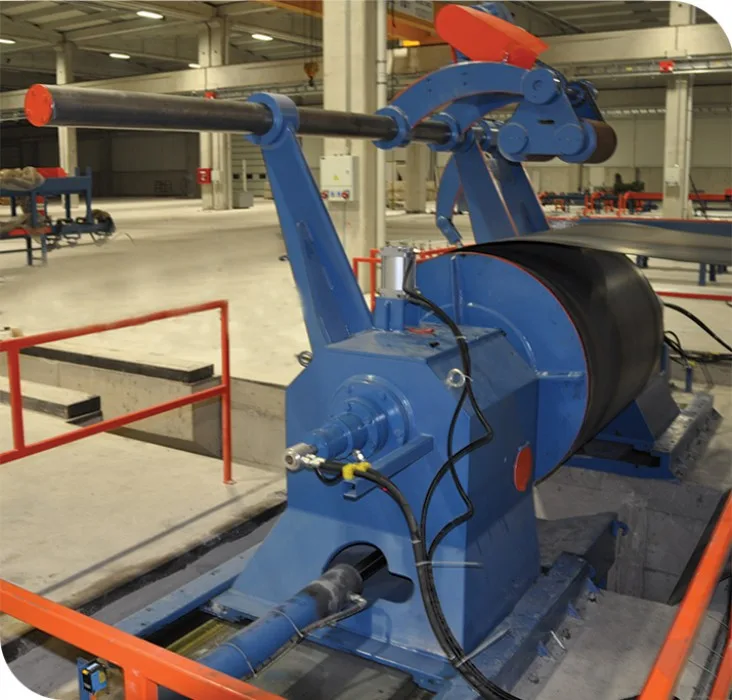
Decoiler
Continuously feeds the coil to the slitting unit. Heads moved by two opposing cylinders clamp the material, and the hold-down roll guides the strip to the next stage.
03 / 09
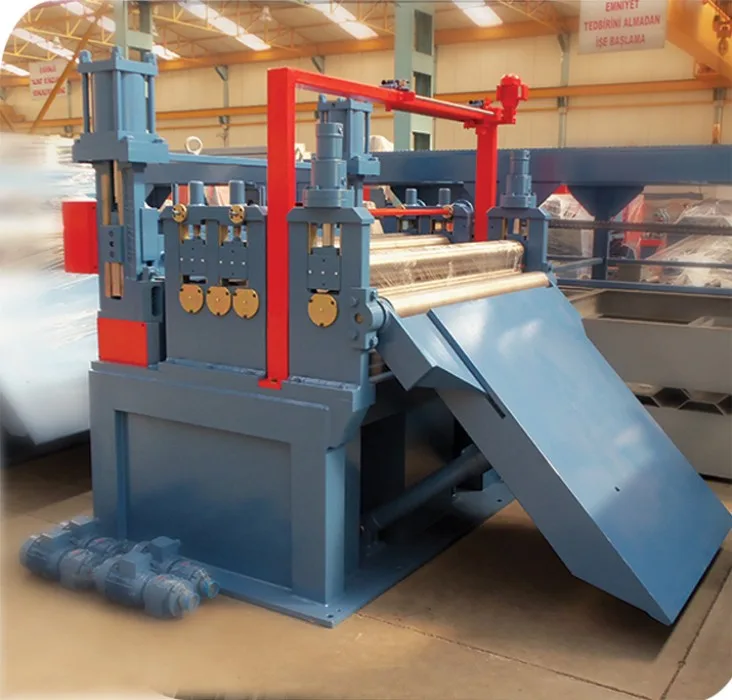
Leveller and Edge Control Unit
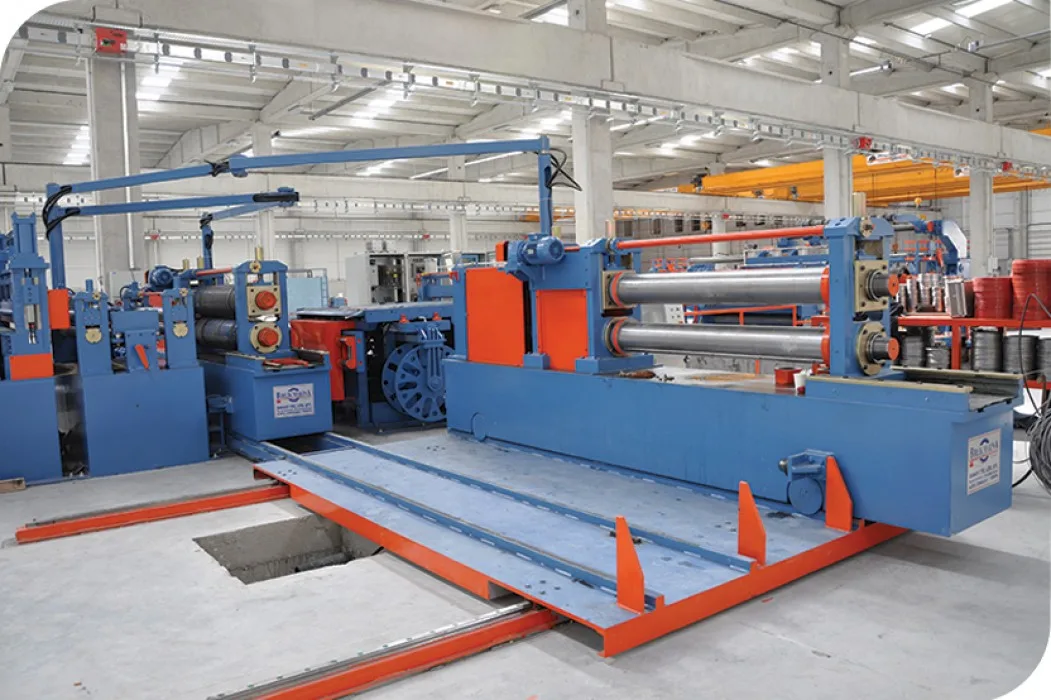
Corrects the deformed parts of the coil coming from the decoiler and prepares it for slitting. It consists of 7 levelling rolls; the first pair acts as pinch rolls. Vertical movement of the upper shaft is hydraulic, rotation is by a geared motor.
04 / 09
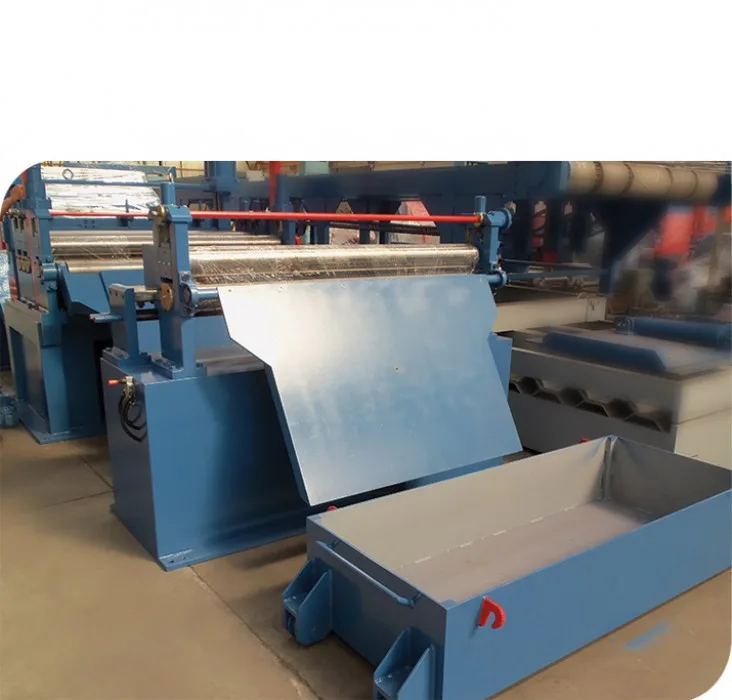
Guillotine Shear
The hydraulic guillotine shear, integrated into the leveller unit, cuts off the damaged head of the coil or cuts the coil at any required point.
05 / 09
Slitter Unit
Rotary knives slit the coil into strips of the required widths. The lower shaft is fixed and the upper shaft moves vertically. The slitter shafts are supported on three steel frames; the outboard bearing moves back and forth for easy knife loading. With the optional second (double) slitter head, the next knife set-up can be prepared while production continues.
06 / 09
Scrap Winder
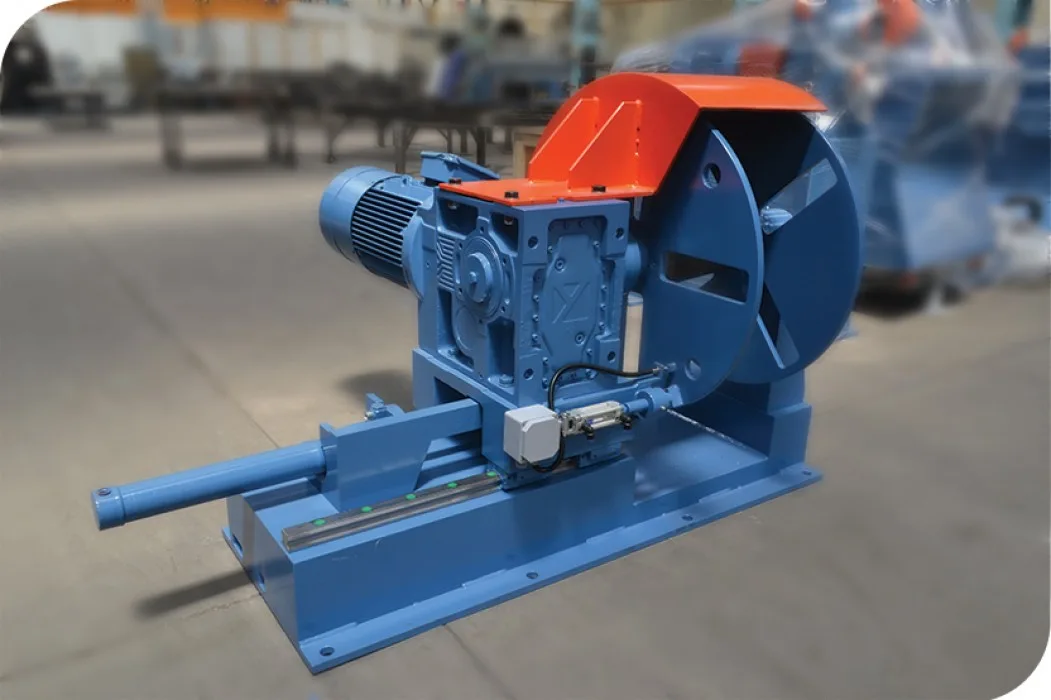
The edge trim from both sides of the coil is wound by two independently operating winders, each driven by a geared motor.
07 / 09
Strip Tensioning Unit
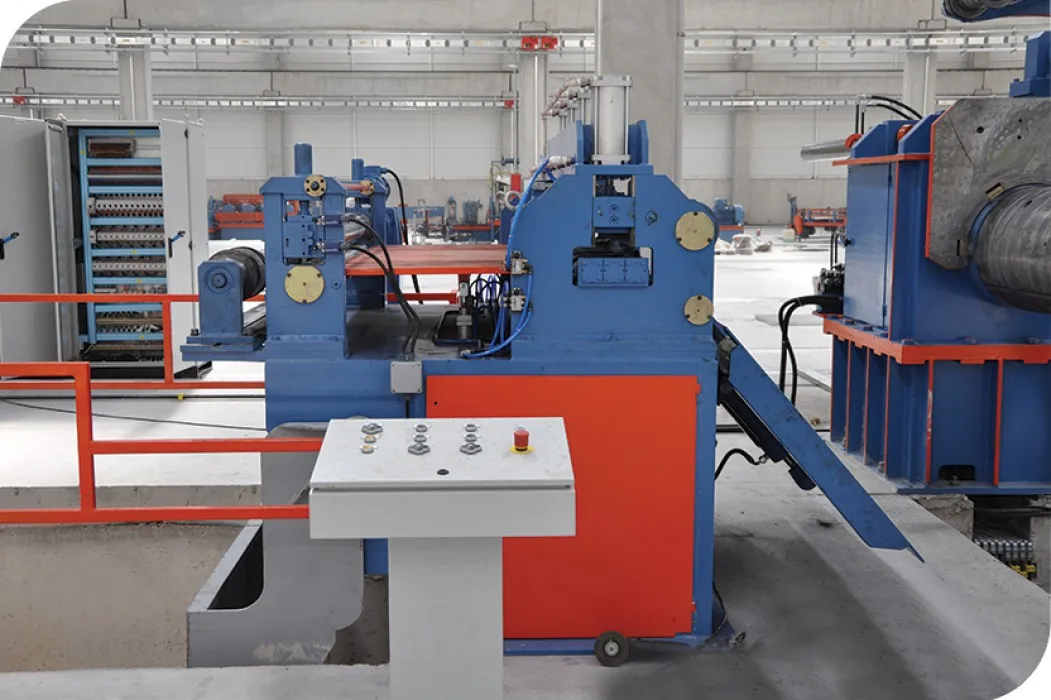
Ensures the slit strips are wound onto the recoiler tightly and evenly. Strips leaving the loop pit reach the recoiler without tangling, guided by separator discs on an idler shaft.
08 / 09
Recoiler
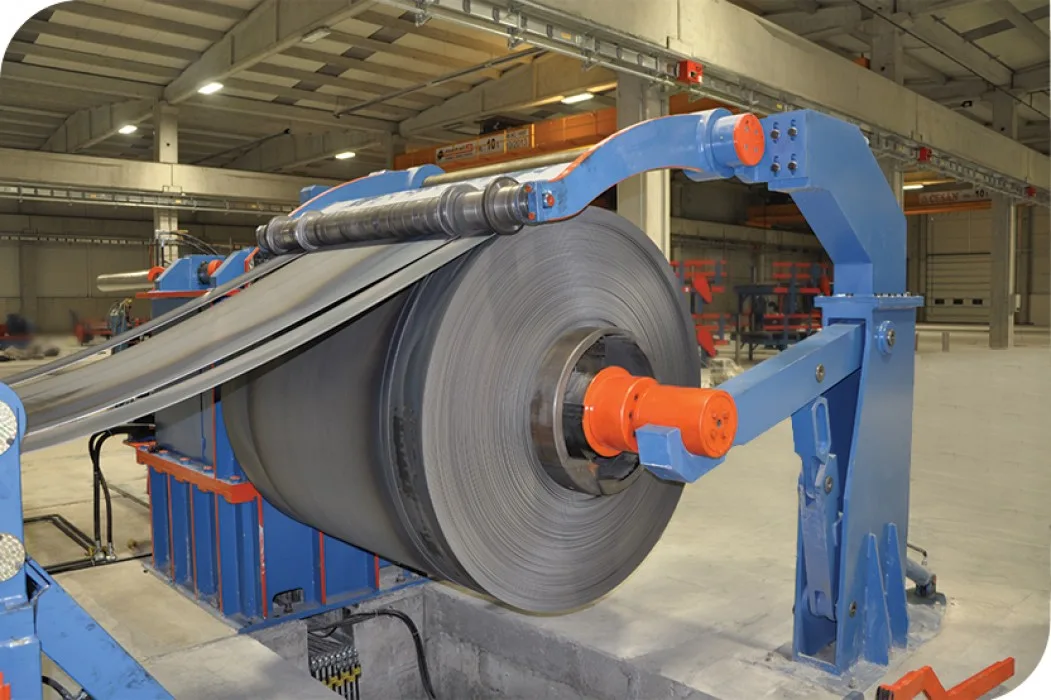
Strip ends are gripped by a mandrel with a hydraulic locking mechanism and wound up; the mandrel diameter expands as it clamps. Separator discs on the overarm prevent strips from tangling. After winding, a hydraulic stripper pushes the coils onto the turnstile.
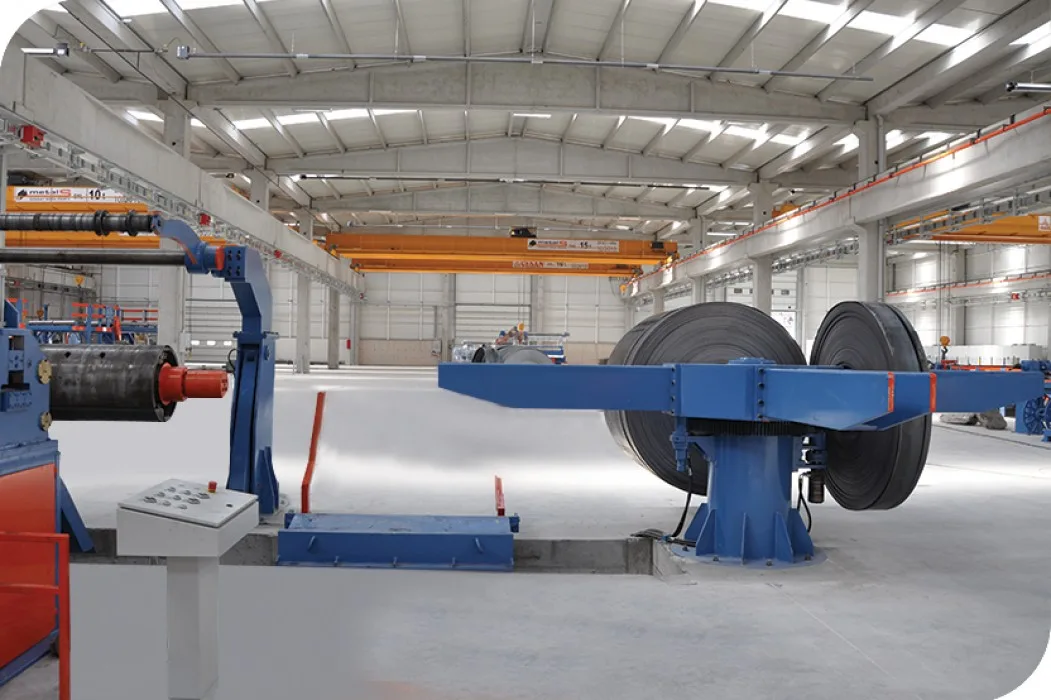
09 / 09
Exit Coil Car and Turnstile
As the stripper cylinder pushes the slit coils off the recoiler, the exit car supports them from below and carries them to the turnstile. The four-arm turnstile rotates on its axis by a hydraulic motor and brings the coils to a position where a crane can pick them up.
Coil Slitting Lines
Videos
Coil slitting line
Steel coil slitting line in production
Coil slitting line 0.80 × 6.00 × 1600 mm
The video loads from YouTube when you press play.
Coil Slitting Lines
Gallery
Coil Slitting Lines
Frequently asked questions
Share your material, product dimensions and capacity target — our engineers will prepare a technical proposal tailored to you.
Which thicknesses and widths can the slitting line process?
Our standard models process coils of 0.50 – 12.00 mm thickness, 500 – 2000 mm width and up to 30 t weight.
What does the second slitter head bring?
With the optional second head, a new knife set-up is prepared on one head while the other is in production. Downtime from knife changes is shortened and capacity rises.
What does the line speed depend on?
Speed depends on sheet thickness and material grade — up to 220 m/min on thin gauges and 40 – 75 m/min on heavy gauges.
Production lines
Other production lines
01
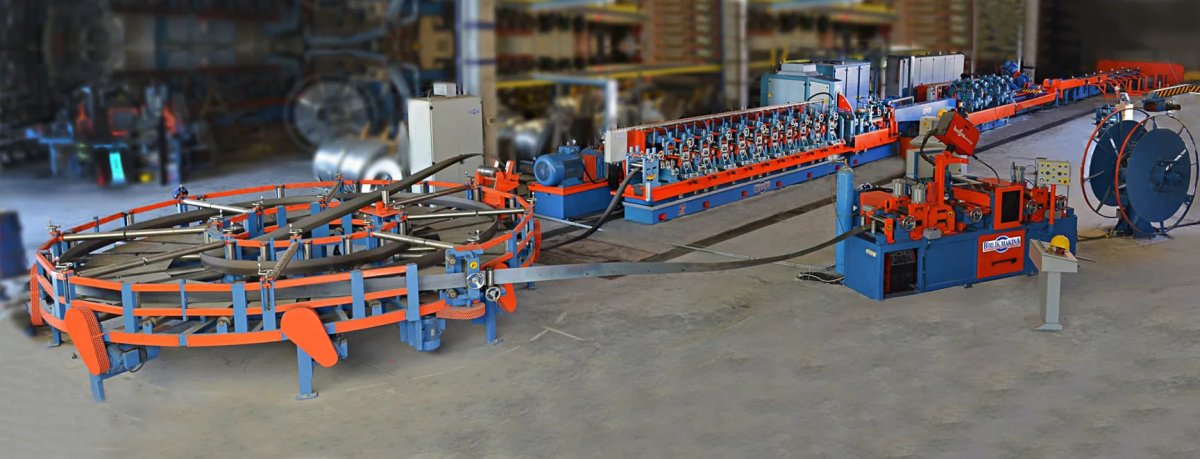
ERW Tube and Profile Mills
Turnkey lines for welded steel tube from Ø10 to Ø406 mm and square/rectangular profiles from 10×10 to 300×300 mm.
- Tube diameter
- Ø10 – Ø406 mm
- Wall thickness
- 0.50 – 12.70 mm
- Line speed
- up to 160 m/min
02
Direct Forming Tube Mills
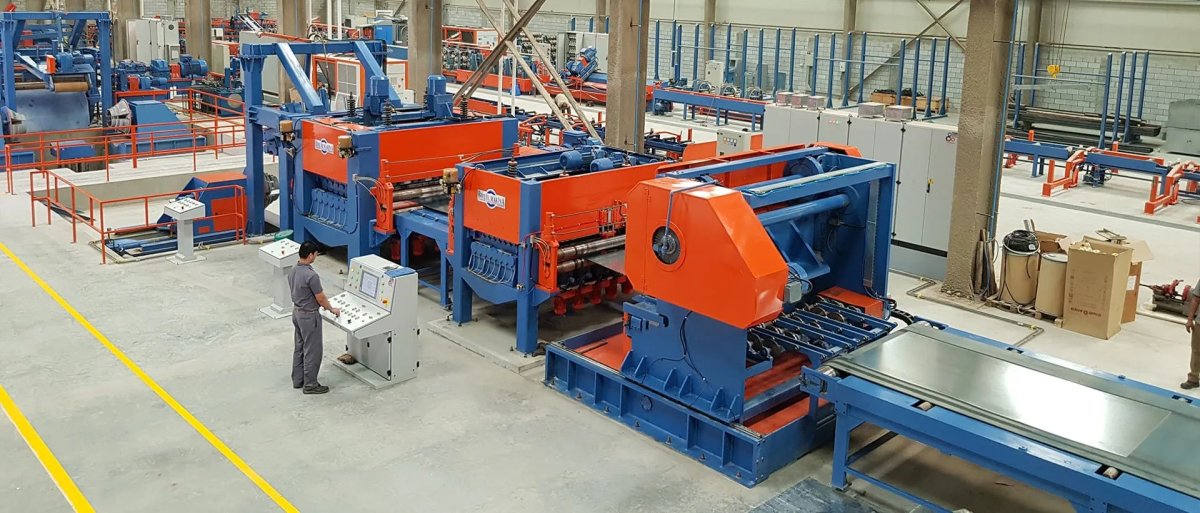
Direct forming lines that produce 20×20 – 120×120 mm square and rectangular profiles with no roll change — sizes are set from the computer.
- Profile size
- 20×20 – 120×120 mm
- Wall thickness
- 1.10 – 6.00 mm
- Line speed
- up to 130 m/min
04
Cut-to-Length Lines
Cut-to-length lines that level 0.50 – 16.00 mm coils, cut them to the required length without stopping, and stack the sheets automatically.
- Sheet thickness
- 0.50 – 16.00 mm
- Coil width
- up to 2000 mm
- Coil weight
- up to 30 t